
Scaling up a tablet from lab bench to full production doesn’t have to be guesswork. Trong thực tế, các tablet scale-up checklist makes sure your R&D recipe works just as well at commercial scale. This means checking every step – the powder mix (xây dựng), the punches and dies (dụng cụ), the press settings (nén), the film-coating process, and the final packaging – before you hit “start” on a large batch. By covering each area methodically, you can avoid surprises and launch on schedule.
Điểm mấu chốt: what works at 1 kg in the lab must work at 1 ton on the floor. That starts with smart formulation work and ends with packing up tablets reliably. In the first phase we confirm the formula and properties (chảy, khả năng nén, vân vân.) are suitable for scale-up. Kế tiếp, chúng tôi prepare the equipment – selecting and qualifying the punch-and-die tooling for the production press. We then run compression trials, checking tablet weight, hardness and throughput at increasing speeds. Once tablets are in spec, we move on to coating adjustments (ensuring lab spray parameters translate to a full-size coater) và cuối cùng choose the right packaging and do stability checks.
In this post we’ll walk through each stage of the tablet scale-up checklist – with tips from industry experts – so you don’t waste time (hoặc sản phẩm) and deliver a consistent, high-quality tablet.
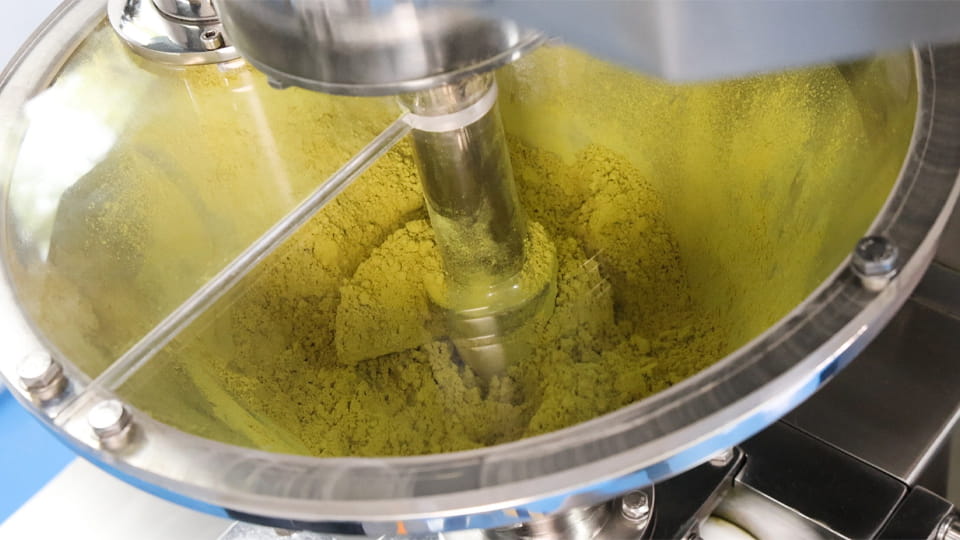
The first step is to make sure your tablet mix is robust enough for scale. Start by confirming the target dose, tablet weight and dimensions based on your API content and powder density. Calculate the needed fill volume and total powder needed per tablet – this guides later mixer and feeder settings. Then do thorough powder characterization: measure bulk and tapped density to compute flow indices (Carr’s index, Hausner ratio), and test flowability (angle of repose or shear cell). This tells you if your powder will feed smoothly through a production feed frame. Be aware that lab tests often use “material-sparing” công cụ (single-punch tablet presses, compaction simulators) to conserve API, but real production presses have very different dynamics (tốc độ, thời gian dừng lại, multiple punches).
Kế tiếp, kiểm tra particle size distribution and tạo hạt chất lượng. If your formula is dạng hạt (ướt hoặc khô), verify that the granules are within spec for size and moisture. A common scale-up pitfall is inadequate chất kết dính or over-dry granules that lead to poor flow or capping. It helps to run screening trials on small equipment (like a lab mill or high-shear granulator) to reproduce your process. Plan time for a small pilot granulation nếu cần: this helps confirm that mixing and drying times for larger batches won’t upset tablet properties.
Another key check is blend uniformity and API content. For potent or low-dose APIs, you should test that your mixing method keeps the API evenly distributed (ví dụ. by assay of blend samples). Content uniformity becomes critical at scale – if you see segregation risk, add a glidant (like colloidal silica) or adjust mixer intensity. It’s wise to measure moisture sensitivity of your mix. A quick humidity test (holding a small batch at high RH for a few hours) can reveal if the powder clumps or sticks, which can cause uneven feeding later.
Document all formulation data: record bulk/tapped density, góc nghỉ ngơi, compaction force profile, vân vân. These feed into a Design of Experiments or risk assessment later. (Regulatory guidelines expect you to identify Critical Material Attributes like these early on.) Cuối cùng, plan an initial small-batch compression on a bench-top or single-punch press. This will give baseline tablet hardness and weight at a given compression force. Keep this data for comparison: as one expert notes, understanding material properties upfront – like compaction curves and friction – is vital for a smooth scale-up.
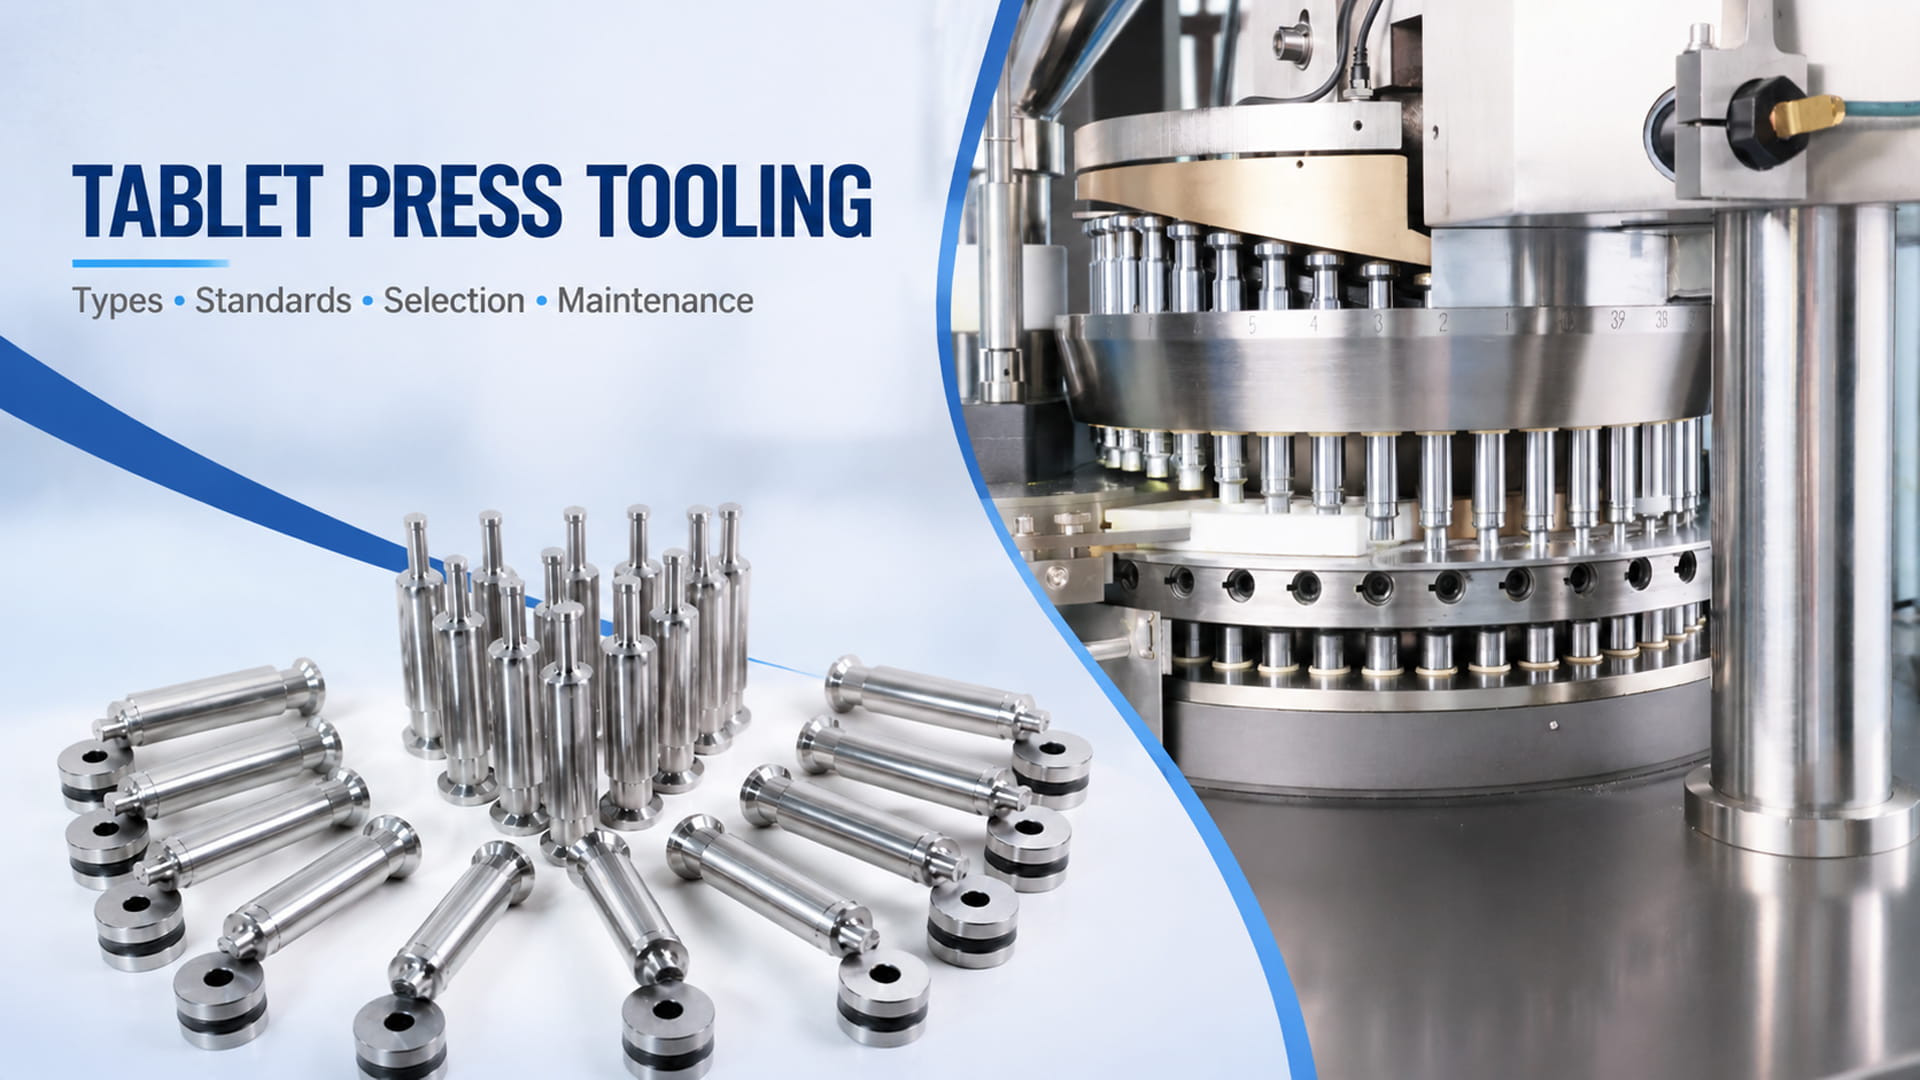
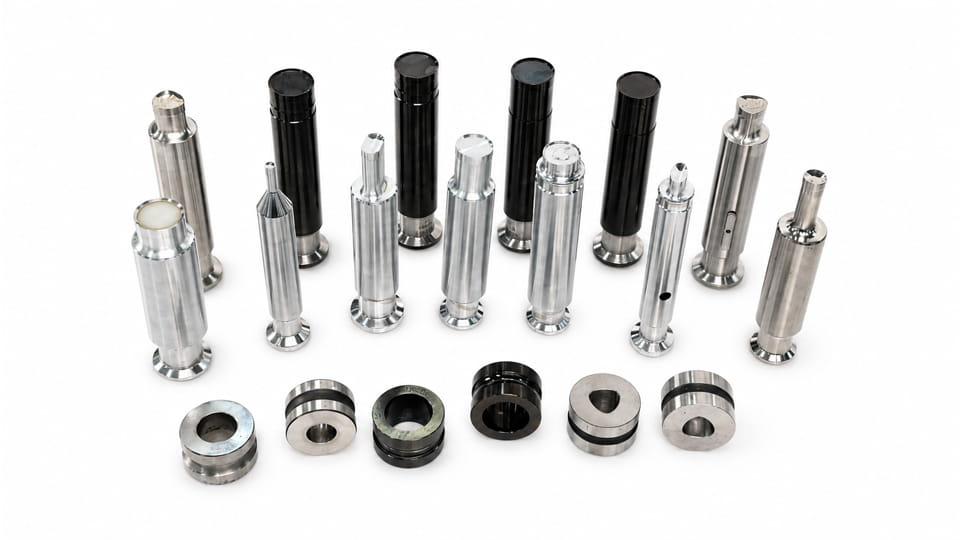
With the formula set, next you pick and verify the dụng cụ (đấm và chết) and get the máy tính bảng sẵn sàng. Choose punches that match your hình dạng và kích thước máy tính bảng (phẳng, biconvex, embossed logo, vân vân.) và vật chất. Most tablet punches are made of hardened steel with a suitable coating (ví dụ. DLC, titanium nitride) for longevity. Ensure the punch depth and die diameter match your tablet’s thickness and diameter targets. (This is often guided by a Tablet Specification Manual or previous product specs.)
Inspect new tooling closely: there should be no burrs, chips or deformations. Clean all parts thoroughly. Install the punches and dies in the production pill tablet press carefully – alignment is critical. Check punch side clearance and tip-to-tip tolerances against manufacturer specifications. Even small misalignments can cause weight variation or punching stress.
After tooling is mounted, perform equipment qualification steps. Conduct an Trình độ lắp đặt (chỉ số IQ) by following the tablet press’s checklist: verify that all safety guards, cảm biến, and software settings are in place, and calibrate the machine’s load cells and displacement sensors. Next do an Trình độ chuyên môn hoạt động (OQ): test the tablet press machine over its range of operating speeds and forces, trigger alarms or interlocks, and make sure emergency stops and feeder controls work properly. Only when IQ/OQ are complete should you proceed to trial runs.
Remember to qualify all relevant tablet-production equipment and auxiliary systems. Depending on your line configuration, this may include the powder feeder, máy tính bảng, máy dò kim loại, and tablet inspection or rejection system. Verify that each applicable component is installed correctly, hoạt động như dự định, and integrates properly with the tablet press. Also establish a BẢO TRÌ and cleaning plan before scale-up trials begin, since even small debris or worn tooling can upset scale-up. Keeping everything logged and “ready” will pay off later in consistent batches.
Now it is time to run tabletting trials on a production-scale tablet press. Do not assume that laboratory settings can simply be multiplied to match the larger machine. Start at a conservative speed, move to the intended production speed, and evaluate performance under representative operating conditions. Ở mỗi giai đoạn, record tablet weight, Độ dày, độ cứng, tính dễ vỡ, and visible defects as appropriate. Use the results to determine whether the process remains consistent as tablet press speed and operating conditions change.
Dùng thử tốc độ thấp: Set the machine to a conservative speed and compression force. Check that each tablet forms cleanly (no capping or sticking). Cân một mẫu thuốc viên (ví dụ. 20 miếng) to verify gross weight, then subtract die fill volume or bed weight to get net powder weight. Ensure weights are within your target tolerance. Also measure hardness and thickness – these should roughly match lab predictions. Inspect tablets for visual defects or tears.
Chạy tốc độ bình thường: Increase to the planned production speed (Ví dụ, whatever output matches your target rate). Run a fixed batch (ví dụ. 1,000–5,000 tablets) and sample periodically. Again check weights, hardness and friability. Chart the fill-weight trend over time – you’re looking for stability (no drift). If you see a gradual drift in weight, look for a cause (ví dụ. hopper feed drying out or a punch walking issue).
Kiểm tra tốc độ cao: If the planned production rate is high, evaluate the press under representative high-speed conditions. Pay close attention to die filling, tablet weight variation, compression behavior, phóng ra, and the occurrence of defects such as capping or lamination. Changes in turret speed and dwell time can affect the compression process, while powder flow and feeder settings may influence die filling. If results become inconsistent, investigate the underlying cause before adjusting the formulation or operating parameters.
Calculate actual output: Don’t trust the press’s nameplate speed alone. Actual tablets per hour = (tốc độ nhấn) × (running time fraction) × (năng suất). A common rule of thumb is to use about 80–85% of the theoretical max speed to account for downtime and changeovers. Ví dụ, if your tablet press can hit 60,000 tablets/hour but typically runs at 90% uptime with a 2% tỷ lệ phế liệu, effective output ≈ 60,000 × 0.9 × 0.98 ≈ 52,920 máy tính bảng/giờ. Use data from your trial (total tablets produced vs. thời gian, minus rejects) to refine this number and size your manufacturing targets.
Throughout the press trials, thực hiện kiểm soát trong quá trình (IPC) for quality. Periodically weigh tablets against USP weight variation limits (for tablets with API). Check a few units for hardness and thickness. Inspect the first and last tablets from each run for khiếm khuyết (giới hạn, cán màng, chip). Throughout the press trials, maintain a documented record of in-process measurements, điều kiện hoạt động, sai lệch, and corrective actions. Trend tablet weight, độ cứng, Độ dày, and other relevant quality attributes over the course of each run. These records will help the team identify sources of variation and support subsequent process evaluation and validation. Ví dụ, if one station is consistently underweight, it may be a tooling offset or a feed issue. Don’t just tweak machine speed – confirm whether it’s a powder flow problem, tooling misalignment, or something else first.
Use this trial to finalize critical process parameters: optimal press speed, lực nén, tốc độ tháp pháo, cài đặt trung chuyển, vân vân. These become your Control Strategy. Make sure operators know how and when to adjust each setting. And remember: what passes for uniform tablet weight in a small run may not hold at scale, so always tie adjustments back to performance data.
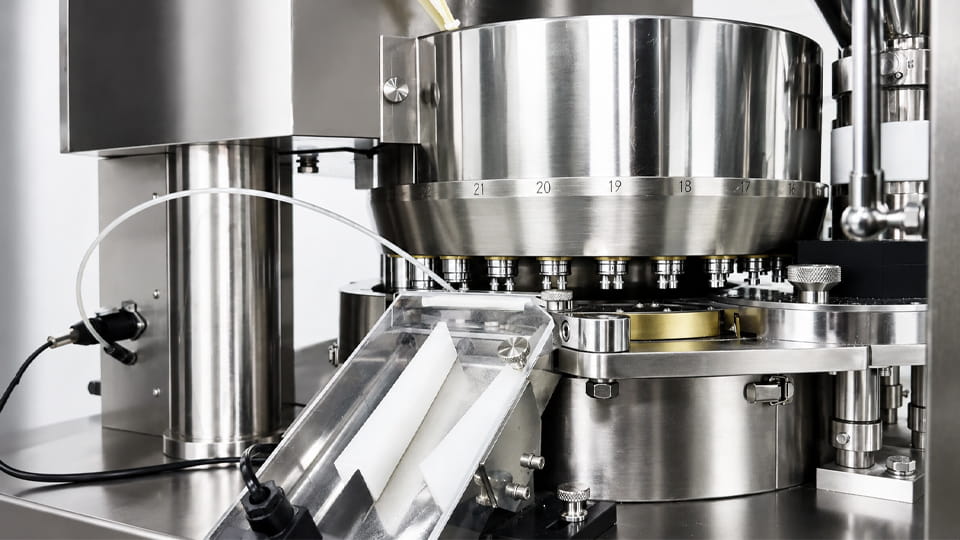
Once viên nén không bao are approved, move on to lớp phủ phim, which often has its own “valley of death” during scale-up. Lab-scale coaters (say 1–5 kg pans) behave very differently from a 500 kg production tablet coater. Here are the main concerns and strategies:
Scale-up Strategies: Several engineering principles can guide you. Đầu tiên, maintain the same Froude number (constant linear velocity) for the tablet bed. Nói một cách dễ hiểu, adjust the pan RPM so the tablets’ motion (speed across the bed) stays the same as in the lab. Thứ hai, always base scale-up on evaporative capacity, như đã lưu ý ở trên. And third, keep as many variables as possible constant (same gun angles, same coating formulation, vân vân.). Nếu có thể, chạy một pilot coating trial on a semi-pilot coater – many companies have intermediate-size coaters (30–50 kg loads) to bridge the gap.
Cuối cùng, plan your coating process parameters through small trials and data logging. Modern lab coaters often have data features; use them to record inlet/outlet air temps, tốc độ phun, và tốc độ quay. Compare these to your target parameters and adjust the big coater accordingly. Tóm lại: scale-up coating by thinking like an engineer – not just “times 100 batch size”, but matching the physics of spray, luồng không khí, and tablet motion.
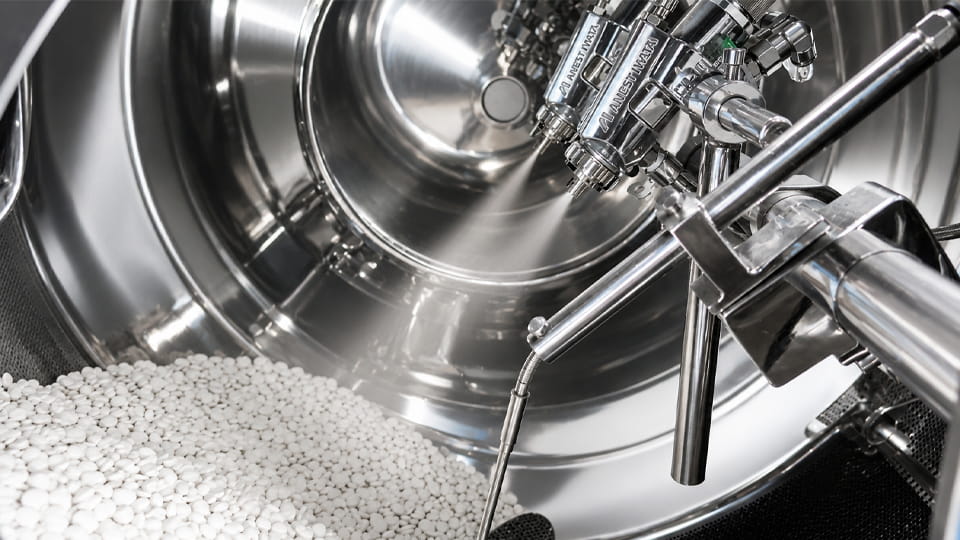
With coated tablets done, it’s time to pick the right bao bì sơ cấp and finalize conditions for stability. The main choice for tablets is often Gói vỉ vs chai (lọ):
Match packaging to your stability data: if a short-term humidity test (ví dụ. 40 °C/75%RH) shows drug degradation, you probably need a high-barrier pack. Regardless of type, make sure the Bao bì line is qualified. Nếu dùng vỉ, install the correct mold/formers for your tablet shape and verify seal parameters. If using a dây chuyền đóng chai, check the cap torque, liner placement and fill-volume settings.
Don’t overlook bao bì thứ cấp – cartons and labels. Schedule a mock assembly with printed cartons and sample labels (với lot numbers or barcodes) to verify fit. Also plan stability studies now: you should begin ICH stability testing in the final intended pack (chai hoặc vỉ) even during scale-up. Accelerated and long-term stability data will confirm your packaging choice.
Tóm lại, packaging scale-up means choosing the form first, then making sure the equipment and materials can handle your volume. Just as with coating, document everything: final container labels, serialization codes (nếu cần), and packaging diagrams should all be completed before full production.
Before you can go commercial, finalize your production plan in writing. This is where FDA and global regulations come in – every change at scale must be tracked. Identify your critical process parameters (CPP) Và thuộc tính chất lượng quan trọng (CQA) from above (Trọng lượng máy tính bảng, độ cứng, coat thickness, vân vân.). Compile these into your batch records and validation protocols.
Follow good documentation practices: Prepare a master batch record template that captures the approved formulation, các bước sản xuất, cài đặt thiết bị, kiểm soát trong quá trình, và tiêu chí chấp nhận. Finalize the relevant standard operating procedures and technology-transfer documents so that the receiving production team can reproduce the process consistently. Document scale-up risks, process changes, sai lệch, and the rationale for any adjustments. Conduct a risk assessment (FMEA or similar) for scale-up changes – this is often required for regulatory filings.
On the regulatory side, be aware of guidances like the FDA’s SUPAC-IR (Scale-Up and Post-Approval Changes for Immediate Release) cho máy tính bảng. That guidance requires that significant changes in scale or process be filed with justification. Ví dụ, if you change the máy tính bảng model or the coating equipment, you may need to show that dissolution and bioequivalence are unaffected. Trong thực tế, this means keeping good data from your trials to show any changes are minor or within proven limits.
As you near commercial runs, complete performance qualification (PQ) on the entire manufacturing line. Before routine commercial production, establish and execute a science-based process performance qualification (PPQ) giao thức. Define the number of batches, sampling plan, tiêu chí chấp nhận, and evaluation methods based on process knowledge, product risks, and applicable regulatory requirements. Document the results and confirm that the process can consistently produce tablets meeting established quality specifications. During PQ, do full testing – weight, độ cứng, giải tán, assays – to ensure every batch meets release criteria. Sau đó, sign off on the process validation report.
Once everything’s in place, perform a final cross-functional review. Involve formulation scientists, kỹ sư, QC analysts and QA. Double-check that no critical factor was missed – that’s the whole point of a checklist. Now your tablet is ready for commercial launch with the confidence of a well-documented, thoroughly tested process.
Tóm tắt lại, here’s a quick actionable checklist for tablet scale-up. Check each item as you go:
By following the steps above, you can tick off each critical factor before full-scale launch.
Scaling up tablet manufacturing is a team effort, but a clear checklist makes it manageable. We’ve covered the essentials – from verifying your formula, to setting up the tablet press, optimizing compression, tweaking the coating process, and choosing the right packaging – with sources and best practices at each stage. Hiện nay you know what to check before committing your product to production.
Ready to make your tablet scale-up smoother? Contact JinLu Packing’s experts for tailored solutions. We offer both lab-scale and production-scale high-speed Máy tính bảng quay nhấn, trình độ cao film coaters, đóng gói vỉ Và dây chuyền đóng thùng designed with scale-up in mind, plus turnkey support. We can even run a production-scale trial of your formulation on our equipment (as part of FAT or pilot testing) to validate capacity and quality. With 3-year warranties and global service centers, JinLu ensures your pharmaceutical line runs reliably. Visit our Máy ép viên page or reach out for a free consultation. Let’s put this checklist into action and plan your next production stage with greater confidence!
Tablet scale-up is the process of transferring tablet production from laboratory or pilot scale to commercial manufacturing while maintaining consistent quality, sự an toàn, và hiệu suất.
Common challenges include poor powder flow, blend segregation, tablet weight variation, compression defects, inconsistent coating, and changes in product quality at higher production speeds.
Good powder flow helps fill the tablet press dies consistently, supporting uniform tablet weight and reliable production. Poor flow can lead to weight variation and inconsistent feeding.
Run compression trials at different force levels and evaluate tablet hardness, Độ dày, tính dễ vỡ, and dissolution. Select a suitable operating range based on product specifications and process performance.
Capping and lamination can result from formulation properties, excess fines, moisture issues, inadequate bonding, or unsuitable compression conditions. Investigate material and process factors before changing press settings.
Not without verification. Production presses differ in speed, thời gian dừng lại, feeder behavior, and compression dynamics, so the process must be tested and optimized on representative equipment.
Evaluate spray rate, drying-air capacity, Tốc độ chảo, spray-gun position, and tablet-bed movement. Adjust the parameters to suit the larger coater rather than increasing every setting in direct proportion to batch size.
Tablets may stick together when the coating spray adds moisture faster than the drying system can remove it. Adjusting spray conditions, luồng không khí, and tablet-bed movement can help reduce sticking.
Base the choice on the tablet’s moisture and light sensitivity, dữ liệu ổn định, thời hạn sử dụng cần thiết, dose format, và nhu cầu sản xuất. Blister materials and bottles offer different levels of protection and operational flexibility.
Depending on the product and applicable specifications, testing may include tablet weight variation, độ cứng, Độ dày, tính dễ vỡ, sự tan rã, giải tán, xét nghiệm, và tính đồng nhất về nội dung.
Tài liệu tham khảo:
1.Phát triển dược phẩm —— Tôi Q8(R2)
2.Dạng bào chế rắn qua đường uống Các vấn đề phê duyệt trước/sau (1/94) —— FDA
3.PAT — A Framework for Innovative Pharmaceutical Development, Chế tạo, and Quality Assurance —— FDA
4.Scale-up of a pan-coating process —— PubMed
5.chương 33 – Phát triển, Tối ưu hóa, and Scale-Up of Process Parameters: Nén máy tính bảng —— Khoa họcTrực tiếp
6.Crystal and Particle Engineering Strategies for Improving Powder Compression and Flow Properties to Enable Continuous Tablet Manufacturing by Direct Compression —— PubMed