×
Service online
✉️E-Mail: 💬WhatsApp: +86 18011793320
💡
  • Heim
  • Blogs
  • Drug Product–Blister Film Compatibility: 4 Key Risks and How to Prevent Them

Drug Product–Blister Film Compatibility: 4 Key Risks and How to Prevent Them

Sicherstellen drug product–blister film compatibility means confirming that the plastic or foil materials used in a blister pack neither degrade the drug nor allow unacceptable interactions. Mit anderen Worten, the film must protect the drug without affecting its quality. The four key risks to check are migration (chemicals moving from film into the drug), sorption (drug ingredients absorbing into the film), statische Aufladung, Und friction. Each of these can undermine stability, potency or manufacturing yield. Tatsächlich, global regulatory guidances treat packaging as a critical quality factor: FDA’s draft guidance emphasizes evaluating container closure systems for drug quality, and ICH explicitly requires stability studies on the drug in its final container–closure system.

Packaging that looks intact may still interact chemically or physically with the drug. Zum Beispiel, plasticizers or inks can migrate out of a film, or moisture can diffuse through a film and hydrolyze a moisture-sensitive API. Ebenfalls, polyester or PVC films can develop static electricity as they unwind, causing tablets to stick or scatter, and poor film flow (high friction) can lead to tearing or misfeeds. These issues aren’t visible at a glance, so systematic evaluation is needed. Broadly speaking, compatibility covers two aspects: chemical/material interaction Und physical handling performance. We’ll explain what each term means and how to assess it.
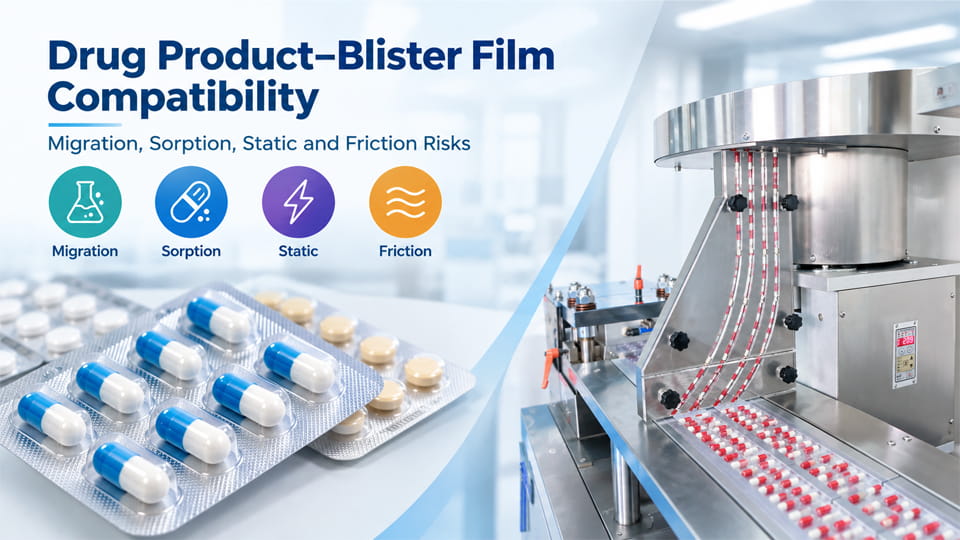
Drug product blister film compatibility risks, including migration, sorption, static electricity and friction, illustrated with pharmaceutical blister packs and packaging equipment.


What Is Drug Product–Blister Film Compatibility?

Drug–packaging compatibility refers to the mutual impact between the drug formulation and the packaging film. It’s not just about barrier performance (moisture or oxygen resistance), but about interaction: will anything leach out, and will the drug leave anything behind? Compatibility also includes processing behavior: can the film be formed, fed, and heat-sealed reliably with the given drug?

  • Packaging vs. Stabilität: In pharmaceutical development, the final dosage form must be tested in its chosen packaging system. Stability problems (assay loss, impurity formation, physical changes) during shelf life can often be traced back to packaging – for example, moisture ingress or light exposure. Blister films serve as a barrier but can also themselves be sources or sinks of chemicals. So compatibility means ensuring the film’s ingredients are inert relative to your API Und Hilfsstoffe.
  • Container Closure vs. Formulation Interaction: FDA’s container closure guidance highlights that a blister pack is a Komponenteof the drug product system. That includes any adhesives, Tinten, oder Beschichtungsschichten. Zum Beispiel, inks on printed PVC film or adhesives on foil lids can be sources of migrants. Auf der anderen Seite, the drug or its solvents might migrate into the film (sorption). All these possibilities need review.
  • Production Fit: Compatibility isn’t only chemical. A film that is chemically inert may still cause jams or defects if, Zum Beispiel, its static charge repels tablets, or its high friction tears on rollers. Mit anderen Worten, Materialeigenschaften (Zugfestigkeit, coefficient of friction, static dissipative characteristics) must suit the blistering equipment and the product’s form (Tablette, Kapsel, usw.).

In der Praxis, evaluating compatibility means answering: “Can this film keep the drug safe Und run on our line?” The rest of this article walks through the four key risk areas.
Tablets and capsules in multiple blister packs, illustrating pharmaceutical product and blister packaging material compatibility.


Risiko 1 — Migration: Can Blister Film Chemicals Enter the Drug Product?

Migration means that substances from the blister film migrate into the drug. Typical sources include polymer additives (Weichmacher, Stabilisatoren, slip agents), Klebstoffe, printing inks, oder Beschichtungen. Even monomer residues or catalysts can migrate. When in contact with the drug (especially if the lid is foil sealed directly to film or if there’s vapor space), these chemicals can leach into the tablets or capsules.

Regulators treat this under extractables & leachables (E&L). ICH’s emerging Q3E guidance and FDA draft guidance stress a risk-based framework for assessing E&L in packaging. In einfachen Worten, migration risk depends on what chemicals are in the film and how harsh the contact conditions are (Zeit, Temperatur). Zum Beispiel, oily APIs might draw out plasticizers, or moisture in a drug could dissolve film components.

A key distinction: Extractables are what you könnte pull out of packaging in laboratory solvents, während Leachables are what actually migrates under real storage/use conditions. Migration tests simulate worst-case conditions (z.B. hohe Temperatur/Luftfeuchtigkeit) and use analytical chemistry to detect any leachables in the product. But you don’t need to do blind screening without context – first conduct a risk assessment by reviewing the film’s composition. Get the material’s spec sheet or coextrusion recipe (often PVC/PVDC/PE layers, usw.), and ask suppliers for extractables data if available.

Practical tip: Suppose you use PVC/PVDC-Folie. PVC may contain phthalate esters and residual vinyl chloride, while PVDC is often coated with organic solvents or plasticizers. Each layer could contribute migrants. Also, risk assessment first: “Does this film or its ink have any known potential leachables?„Wenn ja, plan targeted testing or choose a purer film. Erinnern: relying on the film’s trade name or type isn’t enough – the actual formulation (Dicke, additives, sealant layers) Angelegenheiten.

How to Evaluate Migration Risk

  • Dokumentenprüfung: Gather the film’s “bill of materials.” Identify polymers and additives. Check supplier data sheets or ask for compliance letters (USP class VI, usw.) and any extractables/leachables tests they’ve done.
  • Risk Matrix: Classify leachables by toxicity and likely concentration. An inert monolayer PP film poses less risk than a multi-layer PVC/PVDC film with unknown stabilizers.
  • Lab Testing: If risk is non-negligible, do a leachable study. Expose the closed package to exaggerated conditions (z.B. 40°C/75 % relative Luftfeuchtigkeit) and analyze the content for unexpected peaks (GC-MS, HPLC). Use reference standards or MS libraries to identify any detected substances.
  • Set Acceptance: For any migrant found, perform a toxicological risk assessment. If levels are below safety thresholds, it may be acceptable. Document everything in the chemistry, manufacturing and controls (CMC) aufzeichnen.

Zusamenfassend, you must consider migration early. It’s not enough to pick a film because it’s “standard.” For example, PVC/PVDC films are common but have plasticizers that könnte migrate. So ask: What plasticizer is used, and what is its migration potential? Für sehr empfindliche Medikamente, you might instead choose a high-purity film (like COP/COP or laminated PCTFE) or even Alu-Alu foil to eliminate organic leachables.


Risiko 2 — Sorption: Can the Packaging Material Absorb or Adsorb Drug Components?

Sorption covers the reverse concern: drug or excipient molecules transferring into the blister film. This usually happens by two mechanisms: Absorption (penetrating into the bulk of the polymer) oder adsorption (sticking onto the surface). Both can reduce the delivered dose or alter stability.

Drug sorption is often overlooked unless dealing with highly potent or sticky compounds. Zum Beispiel, lipophilic (greasy) APIs might dissolve slightly into a plasticizer-rich PVC layer. Or volatile actives could evaporate and be captured by a hydrophobic film. Typischerweise, sorption is more a concern for compounds with affinity to polymers – think low-dose APIs, Parfums, or essential oils. Solid tablets usually have minimal direct contact, but fine powders can cling to surfaces.

Warum es wichtig ist: If a small percentage of the API (or a critical excipient) is absorbed by the film, the content uniformity in the blister might fall out of spec over time. Auch, the drug in the film may degrade or desorb later, causing stability surprises. In QC, a soaked-up API would show up as weight loss or lower assay in the tablet, and maybe residue on the film.

Factors Affecting Sorption

  • Drogeneigenschaften: Solubility and volatility. A highly lipophilic drug is more likely to be absorbed into a non-polar polymer. A volatile drug or fragrance might dissipate into film or adhesive.
  • Polymer Characteristics: PVC, zum Beispiel, has a moderate affinity for oily substances. Highly crystalline polymers (wie PET) tend to sorb less than amorphous ones (like PP).
  • Film Additives: Plasticizers or tackifiers in the film can increase sorption by providing a “solvent-like” Umfeld. A film with minimal additives (z.B. ultra-clean COP/COC or PCTFE) will sorb less.
  • Contact Conditions: Longer contact time, higher temperatures, or pressure can enhance sorption. Zum Beispiel, thermoforming can allow molten film to entrap some drug dust more tightly.

Testing Sorption

  • Balance Studies: Pack a known quantity of drug in the blister, age it under accelerated conditions, then measure both the drug and any residues on film. If the tablets lose API that isn’t accounted for by degradation, suspect sorption.
  • Hochleistungsflüssigkeitschromatographie (HPLC)of rinsed film extracts can quantify how much drug has moved into the film.
  • Analytical Surface Scans(z.B. FTIR imaging or Raman) may even detect API on the film surface.

If sorption is significant, solutions include changing the film polymer, adding an inert barrier layer (like a thin PCTFE lining), or altering formulation (z.B. add a coating to the tablet to reduce sticking).


Risiko 3 — Static Electricity: How Electrostatic Charge Affects Blister Packaging

Thin plastic films rubbing against rollers, Panzer, or other surfaces can easily build up statische Aufladung, especially under low-humidity conditions. In a blister line, the PVC or PET film sheet may become charged when unwound, schneiden, or thermoformed. Ähnlich, tablets sliding or tumbling generate their own charge. Static causes surprising problems in packaging:

  • Staub & Partikel: Charged film surfaces attract dust, lint or even tiny fragments of tablet. These contaminants then end up in the Blasenhöhlen or under the seal, raising quality issues.
  • Tablet Misalignment: If a tablet and its cavity carry the same static polarity, they will repel each other. EXAIR demonstrated this: “like the same poles on a magnet, static charges with similar polarity will repel, causing the tablet to be rejected from the blister tray”. In der Praxis, a row of tablets may suddenly all bounce out of their pockets or jam at the fill station.
  • Feeding Disruption: Charged tablets can stick to metal or plastic guides instead of falling into place. A once-steady feed can become erratic, hurting OEE.
  • Sealing Defects: During heat sealing, static can cause films to stick prematurely or shift, leading to incomplete seals or misregistered lids.

Managing Static

Static is a process risk more than a chemical one, but it interacts with compatibility. Zum Beispiel, moisture lowers static (humid air allows charge to dissipate). But adding moisture to control static might worsen drug stability, so balance is needed.

Common static control methods:

  • Ionizers (Anti-Static Bars): These devices blow a stream of air carrying both positive and negative ions onto the film or tablets, neutralizing the charge. They can be installed at critical points (just before forming, before fill, after brush-down). EXAIR’s case study shows ionizers reduced static from thousands of volts to near zero, eliminating tablet rejections.
  • Grounding & Luftfeuchtigkeit: Ensure all rollers, guides and work surfaces are properly grounded. Maintaining room humidity above ~40% can reduce static generation (dry conditions are the worst).
  • Material Choice: Some films inherently generate less static (zum Beispiel, adding antistatic additives or using materials like PETG instead of pure PVC). Film suppliers can sometimes provide a low-static grade.
  • Process Design: Minimize unnecessary rubbing or sliding of film. Zum Beispiel, avoid dragging films over plastic chutes or brushes that increase friction charge.

Static effects are often visible as quality drops. If you see dust lumps on products or hear electric shocks when touching the film roll, investigate static control. Erinnern, this is nicht a chemical compatibility problem – but untreated static can mask or amplify real chemical issues, so it must be addressed in the overall assessment.


Risiko 4 — Friction: How Film Contact Affects Drug and Package Quality

Friction is the mechanical resistance when the film moves against other surfaces (Rollen, Förderer, Werkzeuge) or when tablets move within the cavities. Problems due to friction include:

  • Film Jams or Tears: If the film’s coefficient of friction is too high against a guide rail or drive roller, it can stick and then suddenly release, causing misfeeds or tears. Auf der anderen Seite, too low friction (very slippery film) can cause indexing errors.
  • Surface Abrasion: Rough or sharp edges on molds, guides or brushes can scratch or score the film as it feeds. Scratches can be cosmetic, or they can weaken the film locally. In the worst case, a scratch could become a crack that leaks.
  • Tablet Chipping: A rough rotating brush or tight tolerance can rub against capsules or tablets, especially brittle ones, causing chipped edges or generation of powder. Loose powder inside the blister is itself a contamination risk.
  • Seal Failures: Uneven friction or tension in the film can affect how it seats under the heat-seal head. If a film pulls differently across pockets, the seal pressure may vary, leading to cold spots.

Controlling Friction

  • Smooth Machine Parts: All contact surfaces (Rollen, Nocken, Führungsschienen) should be polished and free of burrs. Use polished stainless steel or hard anodized guides.
  • Correct Tension: Follow equipment guidelines for film tension. Over-tightening a film roll can increase pressure against rollers, while a loose roll can slack and snag.
  • Lubrication/Airflow: In einigen Fällen, a small airflow (through compressed air nozzles) can lift film slightly as it moves, reducing contact pressure.
  • Film Additives: Some films use slip agents (like silicone) to lower surface friction. While these adders can also relate to migration risk, they help consistent feeding.
  • Regelmäßige Wartung: Monitor wear on components. Even a small nick on a roller track can become a major friction point as speed increases.

While friction is often considered a mechanical issue, it does tie into compatibility: if the film tears or jams, production grinds to a halt. Ensuring the chosen film runs smoothly on your specific blister equipment is a form of “compatibility” with the manufacturing process.


How to Evaluate Blister Film Compatibility Before Production

Alles zusammenfügen, compatibility evaluation should follow a stepwise approach:

  1. Gather Film Specs: Review the composition of the forming film and lid film. Identify all layers (PVC, PVDC, PCTFE, Aluminium, usw.) and additives. Ask suppliers for any history of use with pharmaceuticals similar to yours.
  2. Risikobewertung: Based on the drug’s properties (Empfindlichkeit, Dosis, Toxizität) and film composition, rank the four risks. A toxic drug or low-dose tablet, zum Beispiel, makes migration and sorption more critical. A fast, dry operation might make static the top concern.
  3. Laboratory Testing: For identified risks, perform targeted tests. This may include:
  4. Extractables/Leachables study(chemical analysis of aged pack).
  5. Migration challenge(storing drug under stress and testing potency/impurities).
  6. Moisture ingress test(ASTM F1249 or similar to measure MVTR of the assembled package).
  7. Stability study(accelerated/long-term) in the final blister pack.
  8. Material Behavior Tests: Evaluate physical performance. Run the films on a blister line (pilot or actual machine): measure static (a static meter), observe for tablet misfeeds, mark-ups on film, oder Marmelade. Test seal strength and visual defects. Check index accuracy.
  9. Rezension & Iterate: If problems show up, adjust materials or process. Zum Beispiel, if migration peaks are too high, switch to a higher-purity film or change the heat-seal adhesive. If static causes 5% Ausschuss, add ionizers or try a different film.
  10. Document Requirements: Define acceptance criteria. Zum Beispiel, “No unknown leachable > 0.1% of dose” or “Tablet assay must stay within ±2% when packaged.” Also set re-evaluation triggers (z.B. if you change suppliers or formulation).

The idea is not to blindly test every combination, but to make smart choices. Regulatory guidance is clear that you don’t have to do every test on every new drug–package combination if risk is low, but you must justify skipping any test. In der Praxis, doing some basic accelerated tests (even just a 3-month stability run in final packs) is common. It catches many issues early.


How to Select Blister Film for Different Pharmaceutical Products

When choosing a specific blister film, weigh Barrierebedürfnisse against processing needs:

  • Moisture-Sensitive Products: For hygroscopic APIs or tablets, high moisture barrier is key. The best barrier films are PCTFE (Aclar)oder Alu-Alu foil. (Aluminum cold-form foil is essentially impervious.) PCTFE can be laminated inside a PVC film (PVC/PCTFE/PVC) to form a heat-sealable high-barrier film. Uncoated PVC alone is usually not enough for moisture-hygroscopic products. Often the industry’s default is a PVC/PVDC laminated film for moisture-sensitive drug blisters, since PVDC coating dramatically slows water vapor ingress.
  • Light/Oxygen-Sensitive Products: Aluminum-containing packs block light completely and have zero oxygen transmission. Ein Alu-PVC or Alu-PET blister is common for such cases. For opaque protection plus unit-dose convenience, ein Allzeit (Kaltform) Pack is the ultimate choice (it offers essentially 100% barrier to light, Feuchtigkeit, Sauerstoff). Notiz: Alu-Alu packs require special blister machines and are opaque, so you lose tablet visibility. If some visibility is okay, a PVC/PVDC film with an aluminum lidding foil is a compromise.
  • Economy vs Performance: For stable, low-sensitivity OTC drugs, Standard PVC oder PETis often fine – they are inexpensive and run easily. PET has better oxygen barrier than PVC and is recyclable, so it’s popular for “eco-friendly” packs. But even “inert” PET will absorb some moisture over long shelf life, so check the tablet’s stability data.
  • Matching Sealing Requirements: Different films seal at different temperatures and pressures. Ensure your line can seal the chosen film. Zum Beispiel, pure PVC seals easily; PVDC-coated PVC needs slightly higher heat due to the extra layer. Consult your machine vendor for recommended seal settings.

In allen Fällen, don’t assume a film’s barrier rating (like an MVTR or OTR number) tells the whole story. Chemical compatibility is separate: a high-barrier film could still leach plasticizers, and a clear film might be tinted by an API over time. Balance all factors.
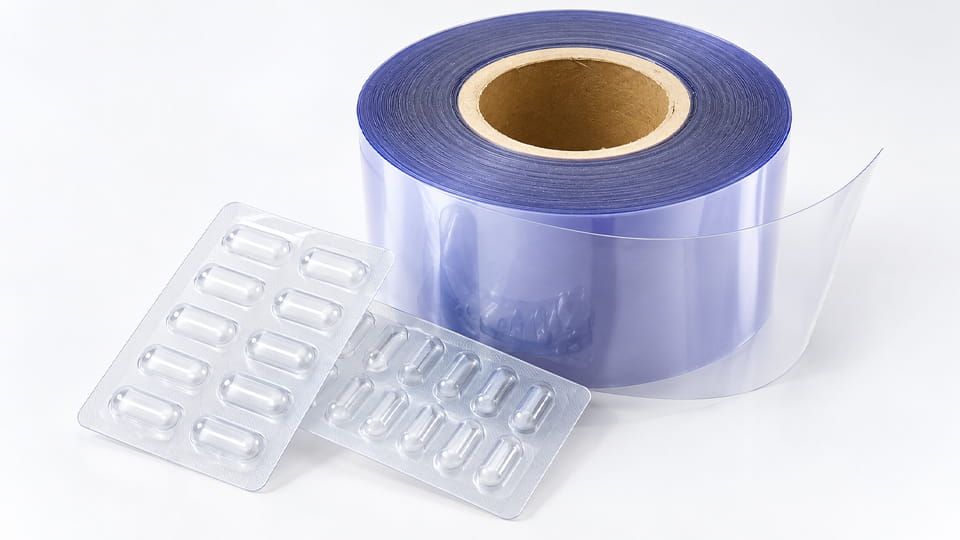
Transparent blister film roll and formed cavities for pharmaceutical blister packaging.

Bild: A roll of transparent PVC blister film with formed cavities. Bei der Bewertung drug-blister compatibility, consider real examples: A commonly used PVC/PVDC film provides good moisture resistance but contains plasticizers that can migrate. A sophisticated PCTFE-lined film gives “virtually no water vapor penetration”, Ideal für empfindliche Medikamente, but costs more and requires lower-speed forming.


Why Verify Compatibility on the Blister Packaging Machine

Endlich, remember that material compatibility must be proven in the actual production setting. A film may pass lab tests but still fail under real machine conditions if not handled correctly. Key process factors include:
  • Umformtemperatur:The heat and pressure used to thermoform the cavities must be optimized for the film. Too high, and the film can over-stretch or polymerize; zu niedrig, and cavities will be malformed or uneven.
  • Cavity Depth and Wall Thickness:Deeper blisters (for large tablets) require more film draw. Some high-barrier films (like PVC/PCTFE or PET) cannot form very deep cavities without tearing.
  • Heat-Sealing:The sealing process requires just the right temperature, dwell time and pressure. These vary by film type. Z.B., PVC may seal at ~140–150°C, whereas PVC/PVDC needs slightly higher, and Alu-Alu needs a different approach. Consistent seals prevent leaks and microbial ingress.
  • Film Feeding and Tension:Stable film transport is crucial. Skew or slack film can lead to misalignment of printed dose numbers or off-center cavities. Make sure the blister machine’s film rollers, sprockets or servo controls match the film’s characteristics.

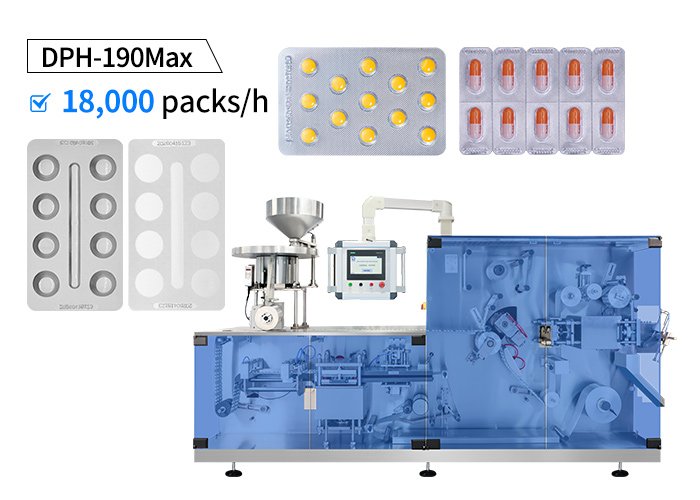
DPH-190Max Hochgeschwindigkeits-Blisterverpackungsmaschine

Figur: Jinlu Packing’s blister machines (z.B. model DPH-190Max) can handle a wide range of blister materials, from PVC and aluminum foil to PET and PS. They integrate precise forming, feeding and sealing controls to ensure consistent pack quality.

Zusamenfassend, run a full machine trial with the chosen film and product before Skalierung. Observe the output packs for defects like incomplete fills, weak seals or foil damage. Only a hands-on trial can reveal issues like film slip or static that weren’t obvious in lab tests.


Common Mistakes in Compatibility Assessment

  • Focusing Only on WVTR/OTR: Barrier numbers are important, but ignoring migration/adsorption risks can lead to surprises. Zum Beispiel, choosing a film solely for its low MVTR might introduce new leachables or static issues.
  • Blindly Trusting Supplier Claims: A supplier brochure may say “USP Class VI compliant,” but that doesn’t guarantee your drugis safe with it. Always verify key interactions via testing or literature.
  • Skipping Machine Trials: Testing only in the lab without trying the actual production line can miss static or friction problems. Always do at least a short run to see how the film behaves on your blister equipment.
  • Not Re-evaluating After Changes: If you change any material – even a different color of film, or a new ink or adhesive – re-run the risk assessment. Minor tweaks can alter migration or static behavior.

Being diligent pays off. Prevention of a quality issue in stability or production is far easier than troubleshooting a complaint or recall.


Abschluss & Nächste Schritte

Drug Product–blister film compatibility is a cornerstone of pharmaceutical packaging design. It ensures that the blister film protects the medication ohne introducing new risks. By systematically evaluating migration, sorption, statisch, and friction risks – and by linking stability data to barrier choices – manufacturers can avoid nasty surprises later on. Always remember that a blister pack is part of the drug product, so packaging and formulation must be optimized together.

For each risk, use the right controls. Chemisch, rely on compatibility testing and stability data. Physically, adjust humidity, use anti-static measures, and fine-tune machine settings. And remember: simulate real production. If a film spills out of the blister forming station or tablets bounce out of cavities on the first run, no lab test could have predicted that.

If you need help matching a drug to a blister film – or setting up your blister machine – Jinlu Packing’s experts are here to assist. We design blister lines that can accommodate all common film types (PVC/PVDC, PCTFE, Allzeit, usw.) while maintaining precise control of form and seal. Kontaktieren Sie uns to discuss your product requirements, or request a trial on one of our Blasenmaschinen. With the right partnership and data, you can prevent compatibility surprises and keep production running smoothly.


FAQs on Drug Product–Blister Film Compatibility

What exactly is drug product–blister film compatibility?

It’s the ability of the blister film and drug product to coexist without adverse interactions. In praktischer Hinsicht, it means no unacceptable migration of film chemicals into the drug, no loss of drug into the film, and no processing problems (statisch, tearing) beim Verpacken. It ensures the drug remains safe and effective while in that blister pack.

What causes chemical migration in pharmaceutical blisters?

Migration usually comes from film additives (Weichmacher, Stabilisatoren) or inks leaching out. Factors like heat (during sealing or storage), Feuchtigkeit, and the drug’s properties (z.B. presence of solvents or oily components) can accelerate migration. Zum Beispiel, heat sealing at too high a temperature might drive more monomers out.

What’s the difference between extractables and leachables?

Extractables are chemicals that could be pulled out of a material under extreme conditions (like using strong solvents or high temp in a lab). Leachables are what actually migrate into the drug under normal or accelerated conditions. In packaging evaluation, you usually analyze extractables first to know what to look for, then check for leachables during stability or migration studies.

How do I know if my drug will adsorb into the film?

Consider the chemistry: is the drug oily or very hydrophobic? These tend to absorb into certain plastics. Also check if the drug dose is very low (micrograms); then even tiny sorption can matter. The best way is an empirical test: store product in the film and measure if potency drops more than expected degradation. Rinse and analyze the empty film for drug content as a check.

Why does static electricity occur on blister films?

Static builds up when insulating films (wie PVC, HAUSTIER) move against surfaces (Rollen, cutters) or when separated (z.B. unwinding a roll). In a dry environment or at high speed, the effect is stronger. Every time a tablet falls into a pocket, a tiny charge can form. Without neutralization, these charges accumulate.

How can static affect the finished pack or production?

Static-charged film can attract dust or fibers which then get sealed into the pack. It can cause tablets to misalign or “jump” during filling (leading to holes or double pills). Static during sealing can even crack tablets if a brush or sensor rubs against the charged surface. Gesamt, it tends to increase rejects and downtime if uncontrolled.

In what way does friction matter for blister packaging quality?

Film friction affects how the sheet moves. If the film sticks too much to a roller, it can break when the machine tries to pull more. If it slips unpredictably, seal alignment can be off. Rough spots on film can mar tablets. High friction on a detents wheel can crunch film edges. So matching the film’s surface properties and tension to the machine is key.

How do you test blister film compatibility without destroying a batch?

Start small. Do lab tests on packaged mini-blisters or individual tablets sealed under lab conditions. Use accelerated aging (hohe Temperatur/Luftfeuchtigkeit) to “speed up” effects. Run a short engineering batch on the actual machine (with sampling) to watch for static or feed issues. Analytical assays can then reveal any migration or potency changes early on.

How do I choose a compatible blister film for tablets versus capsules?

The considerations are similar, but note that capsules (with smooth shells) may slide differently in cavities than flat tablets. You may need slightly higher friction to hold capsules or a shallower depth. For high-barrier needs, both forms can use the same film stacks (PVC/PVDC, PCTFE, Allzeit, usw.). The key is matching barrier to sensitivity: moisture-sensitive capsules or coated tablets often use the same high-barrier films.


Referenzen:
1.Container Closure Systems for Human Drugs and Biological Products —— FDA
2.GUIDELINE FOR EXTRACTABLES AND LEACHABLES —— ICH Q3E
3.Understanding and Characterizing the Drug Sorption to PVC and PE Materials —— PubMed
4.Comparison of solute-binding properties of plastic materials used as pharmaceutical product containers —— PubMed
5.Impact of electrostatics on processing and product performance of pharmaceutical solids —— Monash-Universität
6.Standard Test Method for Determining Integrity of Primary Packaging by Visual Inspection —— ASTM F1886/F1886M-25
Teilen Sie diesen Artikel:
Bild von Kleines Fu
Kleines Fu

Kleines Fu, Gründer von Jinlupacking, bringt vorbei 20 langjährige Erfahrung im pharmazeutischen Maschinenbau. Unter seiner Führung, Jinlu hat sich zu einem vertrauenswürdigen Lieferanten für integriertes Design entwickelt, Produktion, und Verkäufe. Petty teilt mit Leidenschaft sein umfassendes Branchenwissen, um Kunden bei der Bewältigung der Komplexität von Pharmaverpackungen zu unterstützen, Sicherstellen, dass sie nicht nur Ausrüstung erhalten, sondern eine echte, auf ihre Produktionsziele zugeschnittene Servicepartnerschaft aus einer Hand.

Inhaltsverzeichnis

Senden Sie Ihre Anfrage

Hinterlassen Sie eine Antwort

Ihre E-Mail-Adresse wird nicht veröffentlicht. Erforderliche Felder sind markiert *

Holen Sie sich ein kostenloses Angebot

*Wir respektieren Ihre Vertraulichkeit und alle Daten sind geschützt. Ihre personenbezogenen Daten werden ausschließlich für die JL-Lösung genutzt und verarbeitet.