Blisterverpackungs-Scale-Up: Eine vollständige Checkliste für Materialien, Werkzeug, Keimenversiegelung & Validierung
Blisterverpackungs-Scale-Up: Eine vollständige Checkliste für Materialien, Werkzeug, Keimenversiegelung & Validierung
Oktober 26, 2026
Keine Kommentare
Blister packaging scale-up isn’t just turning up the speed on your machine. It meansmaking sure every part of the process works togetherwhen you jump from trial batches to full-rate production. In der Praxis, companies often see new problems arise: seals that used to hold suddenly fail, blister cavities stretch or wrinkle, or foil lids start peeling off. These issues usually trace back to changes in the process – wider machine beds, higher throughput, even minor material variations – that weren’t accounted for at smaller scale. Our checklist cuts through the noise. We’ll show you how to systematically confirm yourMaterialien, Werkzeuge, process parameters and equipmentare ready for commercial production so you maintain consistent quality as you grow output.
Am Ende dieses Leitfadens, you’ll have a clear roadmap – from defining your production goals to final validation – so you can increase your blister line outputwithout compromising unit-dose integrity or throughput. Tatsächlich, the FDA emphasizes that process validation must gather evidence “from the process design stage through commercial production” to ensure a process can “consistently deliver quality product”. Mit anderen Worten, scale-up is part of validation, not an afterthought.
Define the Scale-Up Target and Quality Requirements
Start by setting clear goals.How many blister packs per minute (PPM) do you need? Do you require multi-lane operation? What is the blister format (pocket size, number of cavities, strip length)? Document the product’s dimensions, fill weight and tolerances – for example, tablet diameter/height or capsule length – so tooling can be designed correctly. Also specify your quality targets: allowed defect rate, erforderliche Haltbarkeitsdauer, Siegelfestigkeit, and barrier properties needed to meet stability specs.
Think of this as the foundation: What are you scaling up from, and to what? Zum Beispiel, going from a pilot run of 50 PPM single-lane to a commercial line of 200 PPM four-lane means your throughput goal is 800 packs/minute total. Knowing this up front guides every other decision. It’s also a good idea to benchmark your small-scale performance (z.B. average dwell time, seal peel force, Ausschussquote) as a baseline. That way you can detect any drift during scale-up.
Define production rate:Target packs/minute, Fahrspuren, and shifts. (Z.B. 4 lanes × 60 PPM = 240 packs/min.)
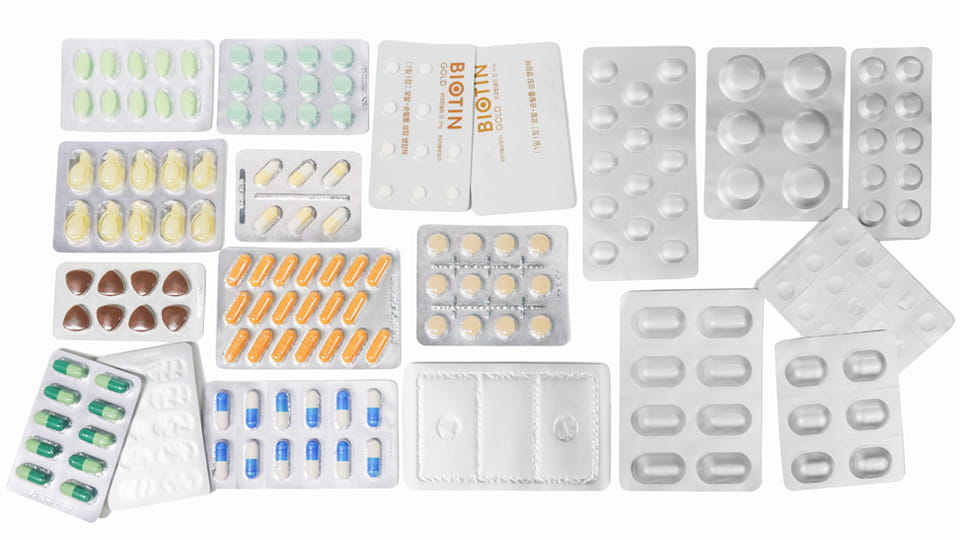
Specify packaging format:Cavity layout, Abmessungen, draw depth, web width, usw.
Set quality specs:Seal integrity, allowable pinholes, dimensional tolerances, Kopfraum, usw.
Align with regulations:Bestätigen Verpackungsmaterialienand processes meet pharmacopeial and GMP requirements.
This step ensures everyone (Maschinenbau, Qualitätssicherung, Produktion) agrees on what “success” looks like. Only after the target is clear should you move on to verifying that materials and equipment can actually achieve it.
Confirm Blister Packaging Material Compatibility
Not all films and foils perform the same at high volume.During scale-up, you must double-check that your chosen plastic web andlidding foilwork well at the intended production rate and conditions.
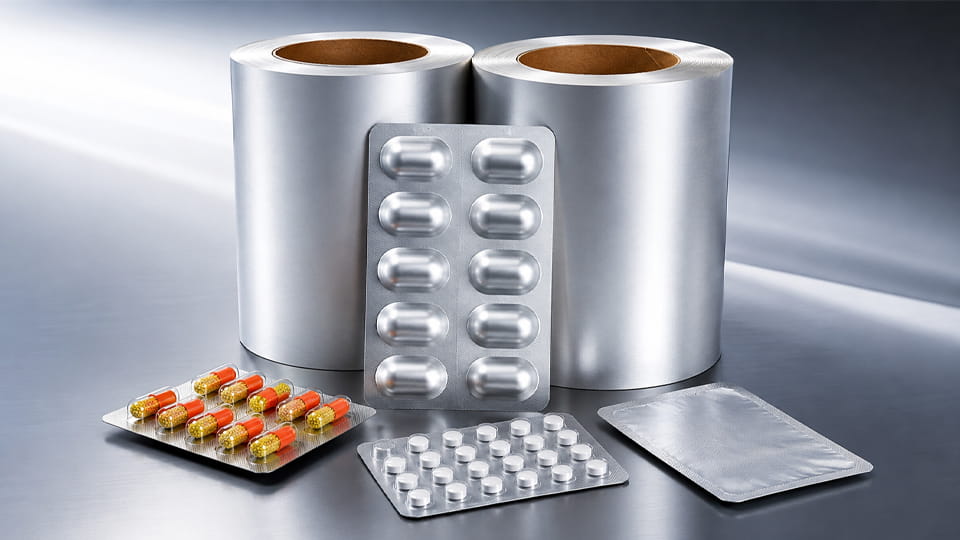
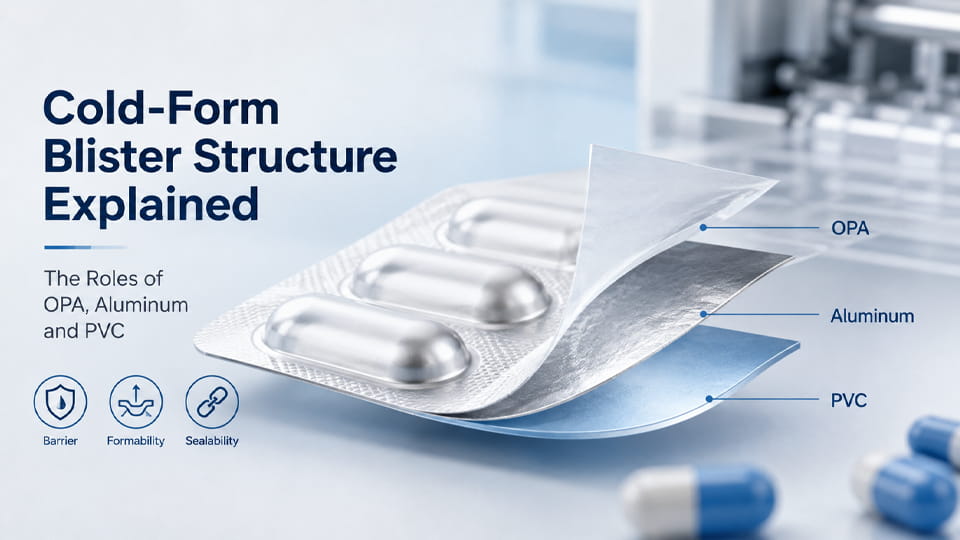
Forming Web (Bottom Film):Zu den gängigen Optionen gehören: PVC (Polyvinylchlorid), PVC/PVDC-Laminate, PCTFE laminates, or other thermoforming films. PVC ist günstig und leicht zu formen, but has limited moisture-barrier. Im Gegensatz dazu, A PVC/PVDC-Folieadds a PVDC coating for much lower permeability. Zum Beispiel, a 250 µm PVC web alone might have a water vapor transmission rate (WVTR) around 3 g/m²·day (38 °C, 90% RH), whereas the same thickness with PVDC typically drops to 0.3–0.6 g/m²·day. PCTFE/PVC laminatesoffer still higher barrier (nearly impervious to moisture) but cost more. Im Allgemeinen, choose a film that matches your product’s stability needs and process capabilities.
Lidding Foil:Most pharma blister usesAluminiumfoliewith heat-seal lacquer. Foils range from ~20 µm (dünn) to 100+ µm (dick) and can be aluminized PET or plain Alu-Alu. Thinner foil is easier to seal and pierce, but thicker foil gives a stronger moisture/oxygen barrier. For critical moisture-sensitive products, fullyKaltformfolie (Allzeit)is often used – it provides a “near-complete barrier for water and oxygen” and long shelf life. (Be aware: cold-formed Alu-Alu requires higher forming force and has no transparency.) Check that your chosen foil’s seal lacquer is compatible with the film. Sometimes a foil requires a specific activation temperature. Obtain and review supplier specs: z.B. PVDC/PVC filmmight seal at ~160–170 °C, while foil might need 170–200 °C.
For both web and foil, insist on materiallot consistency. A material batch that formed fine on small runs can behave differently in long runs if thickness or coating weight vary. Ask suppliers for data sheets showingthickness tolerances, MVTR/OTR (oxygen transmission), and recommended heat-seal conditions. As one example, a PVC/PVDC film spec might list WVTR of 0.3–0.6 g/m²/24h (much lower than plain PVC) and sealing range 160–180 °C.
Endlich, test the materials on a trial machine if possible. Even if they worked on pilot, verifizieren with actual machine hardwarethat the film forms correctly (no thinning or tearing) and the foil seals fully at your target parameters. Document the forming temperature and seal parameters that give defect-free pockets. Erinnern: material choice locks in some limits (z.B. foil thickness vs. peelability), so pick wisely before scaling up.
Validate Blister Tooling and Cavity Design
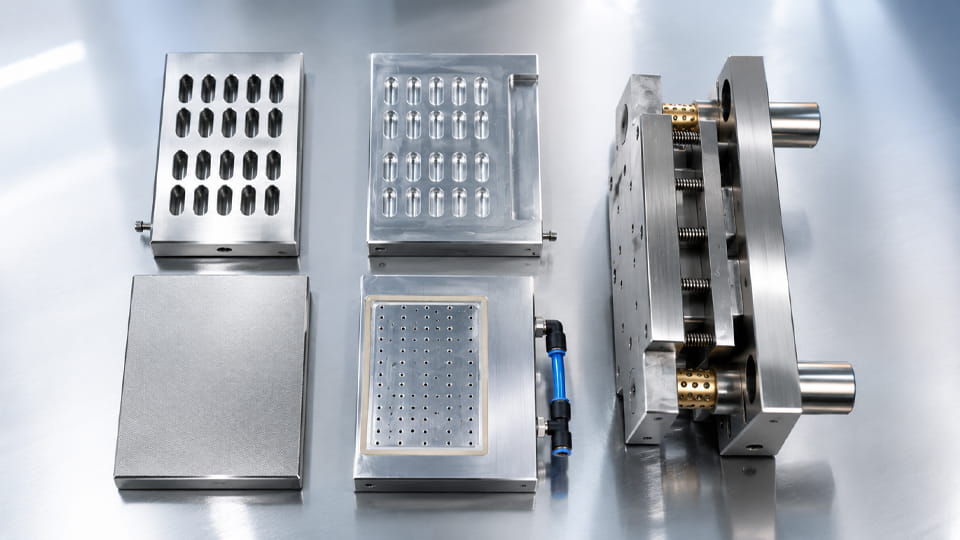
Nächste, ensure your tooling (molds and punches) suits the product and machine. A common scale-up mistake is to assume a lab-sized mold works the same on a faster line – but small misalignments or depth errors can become defects at speed.
Hohlraumgeometrie:Check that each cavity’s dimensions match the product with adequate clearance. Measure tablet/capsule dimensions and compare to cavity width, length and depth. A good rule: allow a 10–20% clearance beyond the part size so the product doesn’t bind or get damaged. Also considerZiehverhältnis (Tiefe vs. base width) – extremely deep blisters (>2× width) can thin the film too much. Normalerweise, pharmaceutical blisters stay under ~2:1. Confirm corner radii are smooth (sharp corners can tear film). If the product sits at an angle, ensure the cavity shape accommodates that (z.B. a slight chamfer for round tablets).
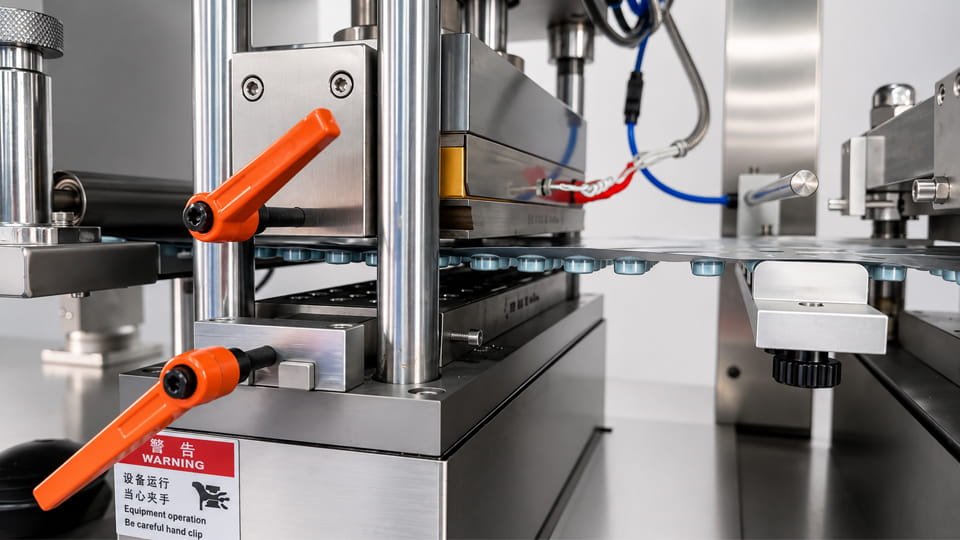
Werkzeugausrichtung:On the actual production machine, verify that the forming mold and sealing plate align perfectly every cycle. Check for any parallelism or centering issues. For rotary machines, alignment of drum stops and cams is critical; for flat machines, make sure the platens align. If using existing molds on new equipment, confirm bolt patterns and platen dimensions are compatible. Also inspect the tooling surface: worn or scratched molds can cause uneven forming and weak spots.
Schneiden und Perforieren:If your blister line punches or separates strips, validate those too. High-speed pistons or blades must be sharp and timed correctly. A sluggish cut at scale can cause jagged edges or web jams.
Predict Maintenance:Scale-up means more runs without idle time. Make sure the tooling material (often anodized aluminum or stainless) can handle the increased wear, or schedule planned maintenance.
Im Zweifelsfall, build a prototype mold (z.B. via CNC aluminum) and trial-run it. Any uneven walls or pop-up are signs the mold needs tweaking. Erinnern: even a well-designed tooling for a single lane might transfer stresses to the machine when multiplied. If you increase lanes (z.B. 2→4 lanes), the frame and drive must handle the extra forming load.
Zusammenfassend, treat tooling validation as an engineering project. You’re essentially confirming that “laboratory-scaled” cavities willSkala– maintaining uniform film thickness and seal area – when run continuously on the production machine. This avoids surprises like thin spots or seal bridges when you hit high speed.
Establish a Robust Forming and Heat-Sealing Process Window
Scale-up success depends on nailing the right processing parameters. Think of this as defining aprocess window– a combination of temperature, Druck, time and speed settings that reliably produce good packs even with normal variation.
Forming Conditions:Start by setting the forming (thermoforming or cold forming) parameters. For thermoforming PVC/PVC-PVDC, preheat zones typically run around 170–190 °C so the plastic is pliable. The forming station then applies vacuum or pressurized air (and sometimes mechanical assist) to draw the plastic into the mold. Typical thermoforming pressures might be in the 4–8 bar range. Ensure heaters across the web width are uniform: multi-lane machines must balance temperature so all cavities form equally. Check the cooling station too – consistent cooling helps the plastic solidify without warping. If cold forming (Aluminium), verify your stamp temperature (usually around 100–120 °C) and that punch force is enough for the foil thickness.
Heat-Sealing Parameters:Diese sind The main variables areSiegeltemperatur, Verweilzeit (contact time), Dichtungsdruck, Und Maschinengeschwindigkeit. A helpful way to see their interplay is this: at higher speed you have less time (verweilen) under the heat platen, so you usually need higher temperature or pressure to achieve the same seal strength.
Sealing Temperature:Typically calibrated per material. Zum Beispiel, a PVDC/PVC film might seal optimally at ~160–170 °C. If the foil has a higher melting point lacquer (or if you switch to thicker foil), the required temperature may rise toward 180–200 °C. Too low a temperature gives “cold welds” (schwache Dichtungen), too high and you risk film bubbling or tearing.
Verweilzeit (Seal Time):This is how long the platen stays down on each seal. Short dwell (fast speed) may not let enough heat penetrate, so seals are weak or incomplete. If dwell is too long, throughput drops and products can overheat. Map out a matrix of (temp vs. Zeit) to find the boundary where seals go from poor to robust.
Druck:Uniform pressure across the entire area is a must. Unequal pressure can leave unsealed spots. On multi-lane machines, check that springs or cylinders are evenly adjusted so all lanes get the same force.
Maschinengeschwindigkeit:Adjust speed after the above parameters are set. The final target speed is tied to production rate, but if you attempt full speed too soon, seals will often fail. Use speed changes to probe the limits of your window.
It’s wise to use aDesign of Experiments (DOE)or systematic trials here. Zum Beispiel, test at mid-range speed and see if the seal passes a strength test. Wenn nicht, tweak temperature or time. Then try a slightly higher speed and adjust again. Record these runs. The goal is to define a range of acceptable values – a “sweet spot” where small fluctuations (±2 °C, ±50 ms, usw.) still yield good seals.
In der Praxis, a table of parameters can help. Zum Beispiel:
Sealing Temperature:Check uniformity ±2 °C; ensure setpoint is stable.
Verweilzeit:Confirm actual platen-down time matches setpoint (short ‘stop’ cycles may reduce actual dwell).
Sealing Pressure:Measure with test foil; adjust if peel is uneven.
Kühlung:On fast lines, check that packs have enough time to cool before being pulled; insufficient cooling can deform packages.
By tuning these on a smaller scale (or in pilot runs), you establish the conditions needed at full scale. FDA-style thinking applies: you’re gathering “objective information and data from laboratory-, pilot-, and/or commercial-scale studies” to ensure the process consistently meets quality attributes. Once you have a stable recipe (z.B. 170 °C, 1.5 s, 5 bar, at 150 PPM), you can move to full-capacity trials.
Check Machine Capacity, Synchronization and Integration
It may seem obvious, Aber verify your equipment is up to the task. A blister pack machine’s nameplate might say “200 PPM”, but actual output depends on many factors.
Capacity vs. Durchsatz:Calculate the actual good-output rate. Zum Beispiel, a 4-lane machine rated at 50 PPM/lane at 10 stations suggests 200 PPM nominal. But if you anticipate a 10% defect and 1 s stop/start cycles, your effective yield might only be 160–180 PPM. For a target of 1200 packs/hour, you’d need at least 7 lanes of 30 PPM. Always plan some margin.
Materialhandhabung:The machine’s hoppers, tablets feeders, usw., must handle the throughput. Make sure your tablet press can supply enough pills per minute. Wenn nicht, you may need a high-speed press or multiple presses. Rotary tablet press machinesare often used in tandem with blisters to avoid starving the line. Ebenfalls, ensure your feeder systems are set up for continuous feed at speed.
Lane Synchronization:Check that all lanes run evenly. Multi-lane machines should have equal transfer timing so that one lane doesn’t lag. Unequal lane speeds can cause gaping film between lanes or misaligned seals. If the machine is electronically controlled, verify the PLC settings; if mechanically cam-driven, inspect cam timing.
Downstream-Integration:Nach dem Versiegeln, packs usually go to inspection and then cartoning. Make sure the downstream line can accept the volume. A slowKartonwill bottle-neck a fast blister machine, causing buffers or stops. Ebenfalls, any in-line printers or date coders must operate at full line speed.
Rejected Packs Handling:Plan for rejects. An often overlooked item is what happens to bad packs. Installing an automatic reject station or scrap chute avoids manual intervention and speed loss.
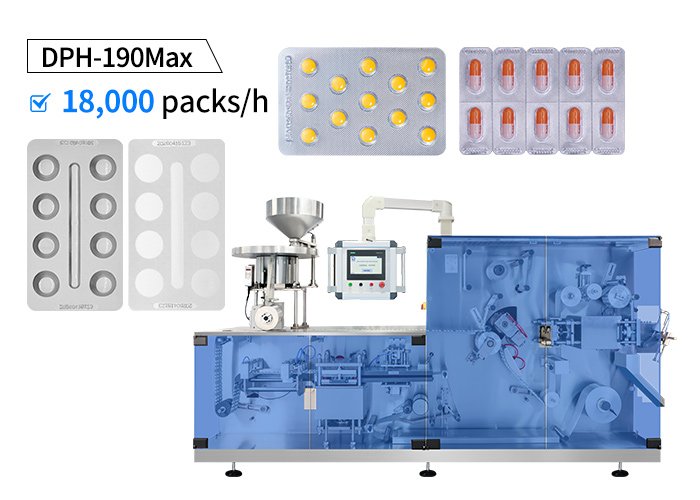
Hochgeschwindigkeitsblasenverpackungsmaschine Linie
Zusamenfassend, match every part of the line to the blister output. This is a good place to consult the equipment manufacturer. Zum Beispiel, JinluPacking’s Blisterverpackungsmaschinencome in various models (einzel- to multi-lane) and can often be customized for your speed and format needs. If your needs are near the top end of a machine’s spec, discuss options like extra feed feeders, additional inspection stations, or even upgrading to a larger machine.
Execute Scale-Up Trials and Troubleshooting
With goals set and systems ready, laufen incremental production trials. Don’t jump straight from 0% Zu 100% Geschwindigkeit. Stattdessen, increase speed in steps, monitoring output at each stage.
Initial Runs:Start at ~50% of target speed using your scale-up recipe. Inspect the first batches closely: do all cavities form? Are seals visually complete (no gaps or wrinkles)? This may reveal if initial heating balance or tooling alignment needs tweaking.
Gradual Ramp-Up:If the first batch looks good, move to 75% Geschwindigkeit, Dann 100%. At each step, inspect quality and measure seal strength. Wenn Mängel auftreten (z.B. seal peeling, cavities not fully forming), adjust parameters incrementally (increase temp, verweilen, usw.) until fixed.
Steady-State Checks:Run at full speed for an extended period (z.B. 30–60 minutes) to see if quality holds. Watch for issues like: film stretching over time, foil starting to wrinkle, or consistency changes. Also note how often the machine stops or how many rejects occur.
Start/Stop Behavior:Blister lines can behave differently when starting up vs. steady-state. Note any anomalies when restarting after a stop (z.B. after maintenance break). Sometimes optimal settings for continuous run differ slightly from those when starting cold.
Dokumentieren Sie alles:Log the speed, parameters, and defect data for each trial. This gives you empirical confirmation of your process window. Zum Beispiel, you might note, “At 100 PPM, seal failure rose above 5% when temperature <168 °C; at 110 °C we regained full seal integrity.”
Fehlerbehebungis key during trials. Häufige Problemeand quick fixes include:
Weak seals or pinholes:Usually fix by increasing dwell time or temperature slightly. Verify that the seal bars are heating as expected (IR cameras can spot cold spots).
Wrinkled or pulled film:Check forming parameters – if the film is too hot/soft or vacuum is high, it can sag. Auch, ensure the web tension is correct (too tight can pull film out of shape, too loose can let it billow).
Foil not adhering or delaminating:The foil might be misaligned or its lacquer not activating. Try adjusting pressure or time, and confirm the foil and film combination is correct.
Machine stalls or jams:Slow feed or heavy rejected load? If jams occur, slow down and check feeding timing. If the machine trips, diagnose mechanical issues before continuing.
Wo möglich, applyDesign of Experiments (DOE)techniques: vary two parameters at a time to find optimal combinations. Even a 2×2 matrix (z.B. two levels of temperature and two of dwell time) can quickly show the safe operating zone. The FDA guidance highlights that you should understand and “control variation commensurate with the risk it represents”. This means if a parameter (like heat) is critical to seal integrity, you must validate its control tightly.
At the end of trials, you should be running comfortably at your target output with defect rates within spec. Wenn nicht, revisit earlier steps (maybe tooling needs change, or a different material).
Complete Equipment Qualification and Process Validation
Before commercial release, treat theBlasenlinieas you would any critical manufacturing process. Follow a qualification and validation program:
Installationsqualifikation (IQ):Verify that the blister machine and accessories are installed per design. Document motor calibrations, heater settings, Sicherheitsfunktionen, usw.
Betriebsqualifikation (OQ):Run the machine through its range of operations (each lane, Geschwindigkeiten, Temperaturen). In OQ, demonstrate that for each parameter (within the range you plan to operate) the machine does what it should. Zum Beispiel, check that set temperatures match actual plate temperatures, that the dosing system distributes tablets evenly, usw.
Leistungsqualifizierung (PQ):Now run actual production (at nominal speed and conditions). This is essentially the last scale-up trial but with formal testing. Use your final recipe and run multiple batches (often three consecutive lots in pharma practice). Test samples from these lots for all critical quality attributes (CQAs).
Key CQAs for blister packaging usually include:
Siegelintegrität:Perhaps the most critical. Use methods like seal peel testing, vacuum leak decay, or dye ingress to ensure seals are hermetic. Zum Beispiel, you might submerge packs in ink after vacuuming to check for pinholes (dye penetration test).
Siegelstärke (Peel Force):Measure the force needed to peel back the foil; it should exceed your spec (often specified by drug regulatory bodies or client requirements).
Cavity Dimensions:Confirm that blister depth and width match design so the product isn’t stressed or too loose.
Aussehen:Visual check for wrinkles, unvollständige Siegel, Trümmer, or foil delamination. Even cosmetic defects are inspected.
Feuchtigkeits-/Sauerstoffbarriere:If critical (z.B. a clinical product), you might perform MVTR/OTR tests on the pack.
During PQ, all parameters must stay within your defined process window. The FDA guidance reminds us that a validated process should have “consistent performance… so that it will consistently produce [Produkte] meeting those attributes”.
Vergiss es nicht Änderungskontrolle: if any element changed during scale-up (new tooling, new material lot, different machine), evaluate whether you need re-validation. In der Pharmaindustrie, even a new material supplier or a different machine lot number often triggers at least partial requalification.
Once PQ is complete with acceptable results, you can move toContinued Process Verification (CPV), the monitoring stage during routine production (Bühne 3 of FDA validation). But that’s beyond scale-up scope. Zur Zeit, your goal is to ensure the line is fully qualified and capable of consistently good output.
Use this quick review checklist before full production:
Production Targets Defined:✔ Packs/min, Fahrspuren, Chargen, and quality targets (Siegelfestigkeit, Fehlerrate) werden dokumentiert.
Material Verification:✔ Bottom film and lidding foil types, thicknesses, and barrier specs are confirmed and meet drug stability needs. Supplier quality docs obtained.
Tooling Design Checked:✔ Cavity dimensions match product with adequate clearance. Draw depths and wall thicknesses reviewed. Tool/mold alignment on the machine has been measured and corrected.
Forming Process Set:✔ Pre-heat, forming pressure, and vacuum settings adjusted so cavities form fully (no thinning or sticking). Forming trials show uniform film thickness.
Sealing Parameters Optimized:✔ Sealing temperature, Druck, verweilen, and speed fine-tuned with actual materials. A robust process window is established (via test runs/DOE).
Equipment Capability Verified:✔ Blister machine (and feeding, inspection equipment) can handle the intended throughput. Multi-lane synchronization and machine speed are tested. Capacity is calculated with expected rejects.
Scale-Up Trials Completed:✔ Stepwise speed-ups were done (50%→75%→100%), with in-line inspections. Settings were adjusted until good seals were maintained at full speed.
Validation Protocol Executed:✔ IR/WH/PQwere performed. Critical Quality Attributes (Siegelintegrität, cavity dimensions, usw.) were measured and met specifications. Final verification reports are signed off.
If all these boxes are checked, you can be confident your Blasenlinieis ready for commercial runs without nasty surprises.
Abschluss
Scaling up blister packaging is a multi-step journey, not a single switch. By following this checklist – from confirming material compatibility and tooling design, through optimizing heat-seal parameters, to full validation – you’rescaling up the processas well as the production speed. That means when you dial up to commercial rates, you’re gettingkonsistent, high-quality blister packsand not a stream of rejects.
Erinnern: the goal issmooth production, not just maximum machinespeed. Mit anderen Worten, don’t rely on the machine’s nameplate speed alone – make sure every subsystem can actually support it. As one of our engineers likes to say, “We’re not just increasing output, we’re maintaining output quality.”
Ready to scale up?Start planning early, involve your packaging equipment supplier in the discussion, and use this guide to stay on track. Contact Jinlu Packaging’s technical teamor visit our website for advice on matching the right blister machine and accessories to your product needs.
FAQs on Blister Packaging Scale-Up
What exactly is blister packaging scale-up?
Blister packaging scale-up means transitioning from lab or pilot runs to full commercial production on blister packaging lines. It involves not just running the machine faster, but ensuring materials, Werkzeuge, heat-seal settings, and equipment capabilities all work reliably at higher output.
Why is blister packaging scale-up challenging?
Because factors that seemed minor at small scale can cause big problems at high speed. Ungleichmäßige Erwärmung, slight film thickness variation, or misaligned tooling might be tolerable in a trial, but at 10× output they lead to seal failures or rejects. Scale-up requires controlling all those variables together.
Which materials are commonly used in pharmaceutical blister packaging?
The forming web is often PVC or PVC/PVDC laminate (for more moisture barrier), or high-barrier laminates like PCTFE/PVC. Lidding materials include aluminium foil (with heat-seal lacquer), aluminium/PET foils, or fully laminated Alu-Alu (Kaltformfolie). Each has trade-offs: PVC is cheap but has moderate barrier, PVDC-coated PVC adds moisture protection, and cold-formed foil offers the highest barrier.
How do you select the right blister packaging material?
Match the material’s barrier properties and formability to your product’s needs. For a moisture-sensitive drug, a high-barrier PVC/PVDC or PCTFE film (low WVTR) with a quality sealant foil is best. Also consider processing: if your process can’t handle too thick a foil, a thinner foil or different laminate might be needed. Always test candidate materials in pilot trials.
What factors affect blister heat sealing quality?
Mainly the sealing temperature, Verweilzeit (contact time under heat), Dichtungsdruck, and the machine speed. In practice these interact: a faster speed means less dwell time, so you might need higher temperature or pressure. Uneven heat distribution or incorrect dwell can cause weak seals or partial delamination. All must be optimized together.
What is the ideal heat sealing temperature for blister packaging?
It depends on the materials. Zum Beispiel, a PVC/PVDC film typically seals around 150–170 °C, whereas certain aluminium lidding foils may need 170–200 °C. The goal is a strong seal without damaging the film. Always run trials: measure seal strength or test leakage at candidate temperatures to find the “sweet spot.”
Why is tooling design important during scale-up?
Because the shape and dimensions of the blister cavities determine how the film stretches and seals. A bad cavity design can cause film thinning or misfeeds at high speed. During scale-up, even a small misalignment or incorrect draw ratio can cause tears. Ensuring the mold fits the product (with proper clearance and draft angles) and is aligned on the machine is key to consistent forming and sealing.
How do you validate a blister packaging process?
Use the standard IQ/OQ/PQ approach. Erste, IQ: confirm the machine is installed correctly (all components in place, kalibriert). Nächste, OQ: run the machine through its operational range, checking parameters (temps, Drücke, Geschwindigkeiten). Endlich, PQ: perform production runs at target conditions, collect samples and test all critical quality attributes (Siegelfestigkeit, Integrität, usw.). This ensures your process consistently meets specifications before release.
What tests are used to check blister seal integrity?
Common tests include vacuum or pressure decay methods, and dye or bubble tests. Zum Beispiel, you might seal a pack, create vacuum, and see if it holds (no pressure rise). Or submerge packs in colored dye or pressurize them with air to spot leaks. Seal strength (peel force) testers are also used. The exact method depends on your setup, but the goal is to detect any pinholes or delamination.
When should I upgrade my blister packaging machine for production?
Upgrade or choose a new machine if your current equipment can’t meet the defined scale-up targets. Signs you need a larger machine include: inability to reach desired packs/minute, frequent jams at speed, or lack of features (Multi-Lane, Inline-Inspektion, Fütterungssysteme). Ideal, assess equipment capability early – if a single-lane lab machine can’t hit needed throughput, you may need a 4- or 6-lane commercial blister machine. Manufacturers can advise which model meets your speed and format requirements.
Kleines Fu, Gründer von Jinlupacking, bringt vorbei 20 langjährige Erfahrung im pharmazeutischen Maschinenbau. Unter seiner Führung, Jinlu hat sich zu einem vertrauenswürdigen Lieferanten für integriertes Design entwickelt, Produktion, und Verkäufe. Petty teilt mit Leidenschaft sein umfassendes Branchenwissen, um Kunden bei der Bewältigung der Komplexität von Pharmaverpackungen zu unterstützen, Sicherstellen, dass sie nicht nur Ausrüstung erhalten, sondern eine echte, auf ihre Produktionsziele zugeschnittene Servicepartnerschaft aus einer Hand.