
In pharmaceutical equipment purchases, many QA and equipment engineers make two mistakes with FAT. Birinci, they only check paper documents and do a simple no-load run. Saniye, they skip special performance checks for model-specific structures. The 45D, also known as a pill press machine, hap presleme makinesi, pill presser, or pill compressor, uses dual compression and dual discharge. Both structures need dedicated verification.
What is factory acceptance testing(YAĞ)? It is a structured verification done at the manufacturer’s site before shipment. . HGZP-45D tablet press structure is complex. Factory acceptance testing must cover documents, mechanical assembly, safety and electrical systems, special mechanisms, load testing, uygunluk, and deviation closure. FAT factory acceptance testing must also verify model-specific structures, cGMP uyumluluğu, Ve 21 CFR bölümü 211 requirements item by item.
Once the equipment is packed and shipped by sea, structural defects are expensive to fix. Rework and part replacement take a long time. Extra cost appears, and production startup gets delayed. Bu yüzden tablet basın makinesi FAT must be thorough. It solves most hidden risks before the machine leaves the factory.
Documents are the input basis for SAT and IQ/OQ work. Check every configuration item against the URS. This prevents mismatched delivery. Before you start, learn how to create an effective factory acceptance test checklist that covers every model-specific item. A clear factory acceptance test checklist keeps all verification steps traceable.
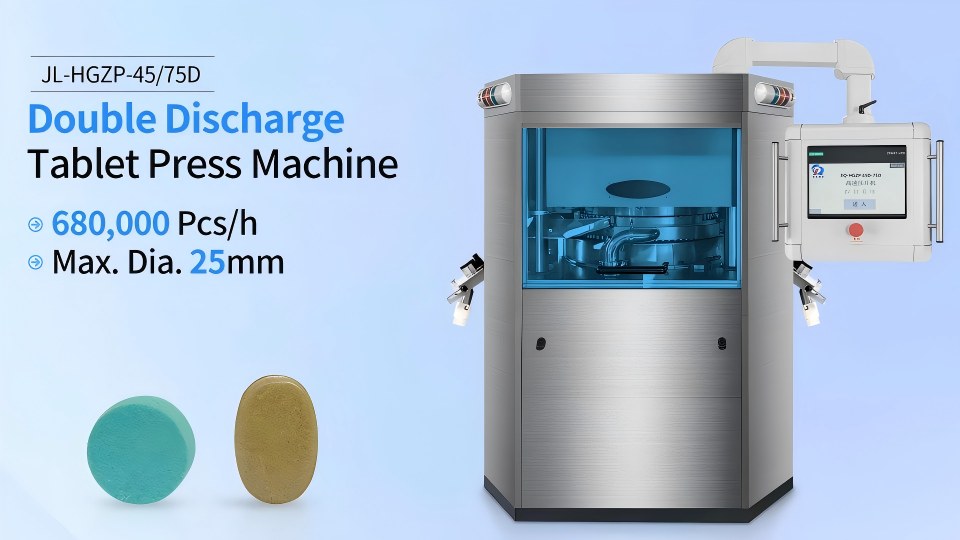
Verify the whole machine model, the 45-punch die count, dual compression mechanism, dual discharge, zorla besleyici, and dust removal system against the contract. Contact parts must pass 316 paslanmaz çelik material verification. Parts contacting the product adopt 316L stainless steel, offering excellent corrosion resistance. The whole set follows the stainless steel ss 316 grade standard stated in the contract. Pressure and temperature instruments need testing and calibration. Lubricants must carry NSF H1 certification to meet pharmaceutical lubrication control requirements.
Collect electrical schematics, pneumatic diagrams, lubrication diagrams, and the full spare parts list. Deliver the operation, Bakım, and cleaning SOP manuals. Include the factory acceptance testing pd folder with protocol documents, test kayıtları, ve kalibrasyon sertifikaları.
For North American export projects, confirm the HMI version and audit trail functions. These must fit 21 CFR bölümü 11 computerized system requirements.
Mechanical checks are not only about a clean appearance. Check tablet press assembly precision, moving parts, and lubrication risk points.
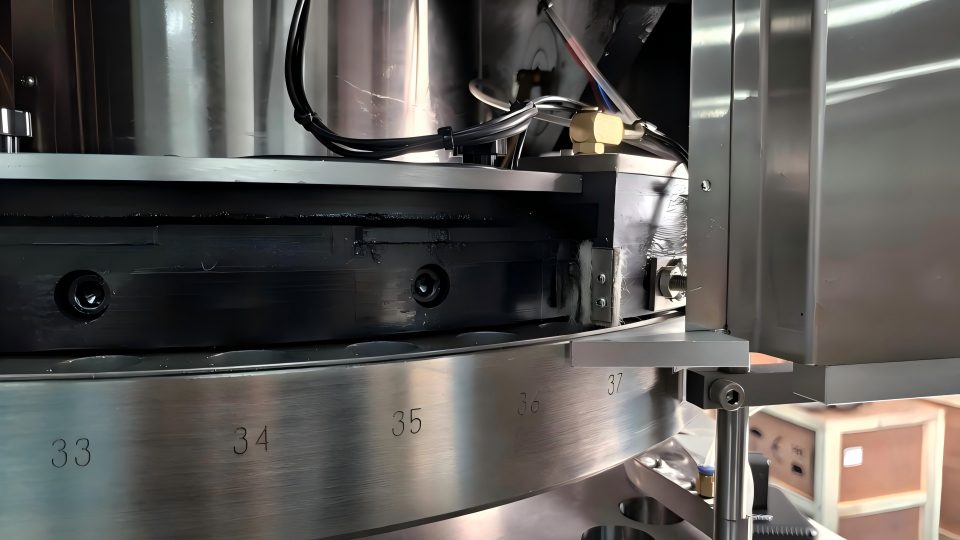
Material contact surfaces must have no burrs or scratches. Measure the turntable runout. Pre-compression and main compression roller assemblies must be tight, with no looseness. The two dual-discharge baffle sets and flow divider parts must be installed correctly and move smoothly. . zorla besleyici and punch assemblies should be easy to disassemble, with no cleaning dead corners.
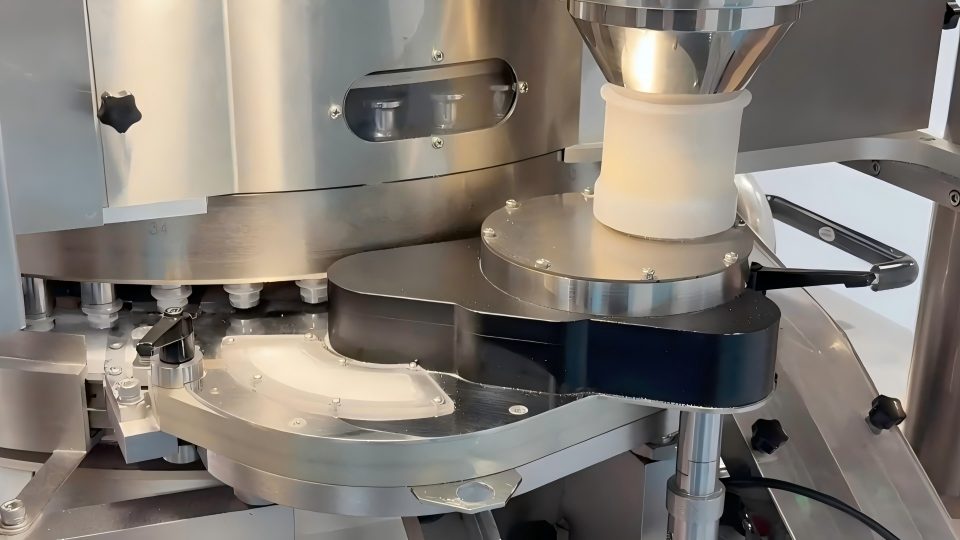
On the HGZP-45D pill tablet press, never apply grease to the middle of the guide rails. Oil is only supplied to the bearings and gear points on both sides. Confirm each lubrication point at FAT. This stops yağlayıcı from leaking into the material area, toplantı 21 CFR bölümü 211 gereksinimler. Check all pneumatic fittings for leaks at the same time.
Complete a full set of tablet press molds disassembly demonstration on site. Confirm the changeover runs smoothly and fasteners lock reliably. Simulate a material change production condition. Check how easy it is to remove product-contact parts. Evaluate cleaning, blowing, and rinsing access. Confirm no powder-hiding sanitary dead corners. This reduces cross-contamination between batches and fits multi-product changeover needs.
Safety interlocks are a hard acceptance item. Many faults only appear under abnormal conditions. Do not skip these tests.
The no-load running test is only a basic judgment. It does not represent production performance.
Run at three speeds: Düşük, rated, and maximum. Each run lasts no less than 30 dakika. Observe overall noise and temperature rise. Pikap, sıkıştırma silindirleri, and feeder should run without abnormal sounds. Perform comparison between set speed and actual speed. Verify the automatic lubrication cycle and the dust removal fan start and stop.
Not: a no-load run only proves the pill press can rotate. Passing it does not mean production with material will pass. Core performance depends on the two special tests below.
This is the most critical part. It separates the HGZP-45D from ordinary tablet presses. On many machines, screen parameters can be changed, but the real mechanism does not work.
The HMI must allow independent setting of pre-compression and main compression pressure. Recipes can be saved and recalled. Modify the pressure parameters and confirm sensor readings change together. Trigger pre-compression and main compression overload separately. Verify the protection shutdown works.
Combine this with a load test. Compare tablet hardness with pre-compression on and off. This proves the pre-compression mechanism actually works. It is not just a value shown on the screen.
Open the 1# discharge and 2# discharge separately. Then open both channels together. The mechanisms must move smoothly and material collection must work. Discharge baffle positions must be adjustable and lockable.
At the load stage, take the tablet in tablet press samples from the two outlets separately. Compare weight, sertlik, and thickness consistency. If the deviation between the two channels is too large, finished product grading becomes difficult. This is a key failure item for the 45D.
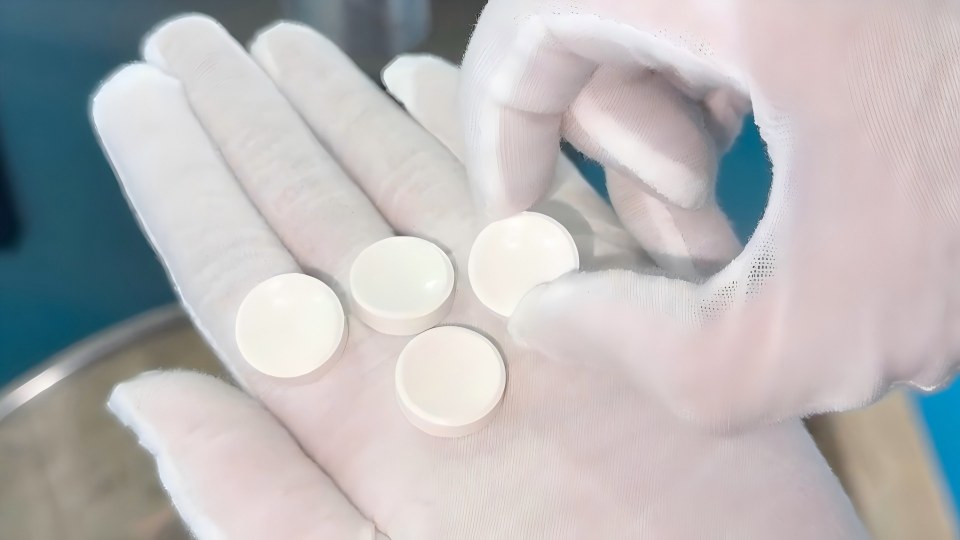
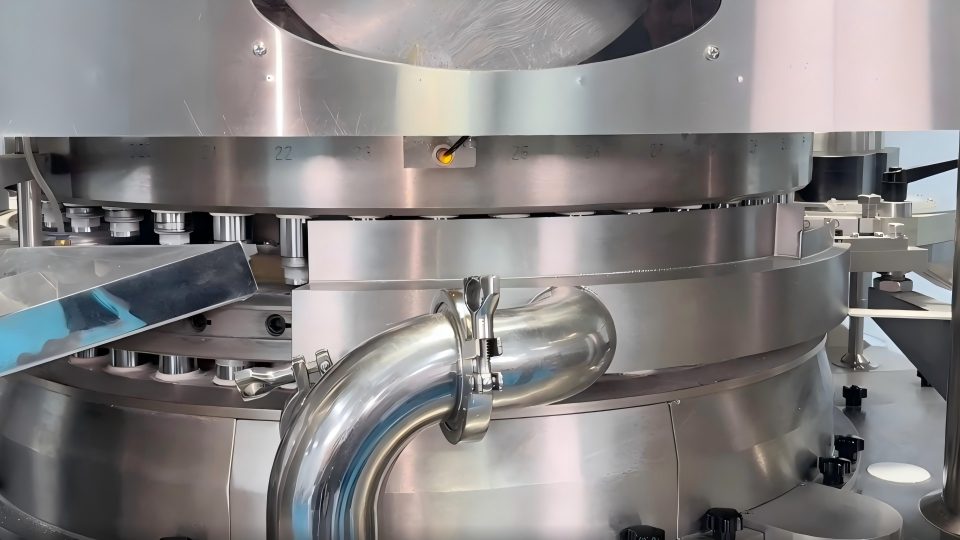
Use simulated granules for the load test. Run at multiple speed settings to fully simulate production conditions.
Complete recipe storage and recall tests, and alarm event recording. For North American export projects, test the audit trail. Demonstrate quick disassembly of the feeder, yumruklar, and discharge parts. Evaluate cleanability to meet cGMP requirements.
Fill in actual measured data for all factory acceptance test checklist items. Judge each item honestly as pass or fail. If problems appear, record the deviation number, fault description, and corrective plan. Close them before shipping.
For validation items that cannot be finished at the factory, mark them clearly. Leave them for key review at SAT on the customer site. The factory acceptance test report requires signatures from both parties. It serves as an important input document for the customer’s on-site IQ validation.
Not: Passing no-load test ≠ production‑ready performance. Proceed to model‑specific and load testing.
The core of the HGZP-45D FAT factory acceptance test is targeted verification. It is not routine signing.
Focus on two special structures: dual compression and dual discharge. Put simulated load testing and cGMP compliance checks into real practice. Many companies treat FAT as a simple process. After arrival, they find pre-compression failure, uneven quality between two channels, or non-compliant lubrication. This costs time and money.
Stopping risks at the factory protects later validation and shortens the startup cycle. Jinlu Packing pill press products have sold to 85 countries worldwide. The machine design follows cGMP standards. We provide on-site commissioning service per project needs. With stable hardware and full-process service, we help pharmaceutical users complete acceptance and production startup smoothly.