
Consistent tablets require control of four key quality attributes: масса, твердость, толщина, и рыхлость. These physical tablet quality attributes (CQA) play important roles in dose consistency, механическая прочность, and downstream performance, включая планшетное покрытие, упаковка, и выпуск наркотиков. But controlling one property does not guarantee overall tablet quality. A tablet can meet its target weight but still be too soft, too thick, or too fragile to withstand handling. Increasing compression force may improve hardness and reduce friability, but it can also decrease tablet thickness and affect disintegration or dissolution. The goal is not to maximize one property at the expense of another. It is to keep all relevant tablet quality attributes within their established ranges while maintaining consistent production.
Так, how do you achieve that balance? You need to understand how powder properties, начинка, предварительное сжатие, main compression force, и скорость башни influence tablet quality. This guide brings those relationships together in a practical CQA map, explains how to troubleshoot conflicting quality results, and shows how the right tablet press configuration can help manufacturers maintain consistent tablet quality at production speed.
In Quality-by-Design terms, а Critical Quality Attribute (CQA) is any property of the drug substance, вспомогательные вещества, or drug product that “should be within an appropriate limit, range, or distribution to ensure the desired product quality.”. For solid oral tablets, typical product CQAs include potency (дозировка), растворение, стабильность, и что немаловажно physical attributes like weight uniformity, твердость, толщина, и рыхлость. These attributes affect purity, сила, and drug release.
Вместе, these four CQAs – weight, твердость, толщина, friability – form the primary physical performance profile of a tablet. They link back to upstream material attributes (например. поток порошка, размер частиц, binder levels) and process parameters (например. глубина заполнения, силы сжатия, скорость). Later, we will present a CQA map that connects raw material traits and process variables to each tablet attribute. But first, let’s see how these four attributes influence each other.
These tablet attributes are not independent. Changes to one often ripple into the others:
Given these interdependencies, we recommend mapping out the relationships. The diagram below (а CQA map) illustrates how key material attributes and compression parameters influence each tablet CQA:
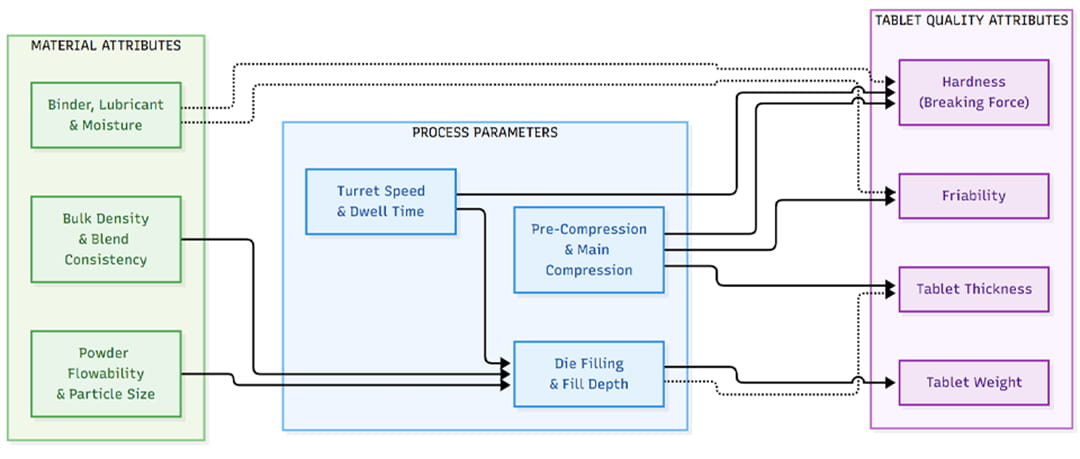
Фигура: How tablet weight, твердость, толщина, and friability are related during compression. Текучесть порошка, размер частиц, объемная плотность, and formulation characteristics influence die filling and compaction behavior. Process parameters such as fill depth, сила сжатия, скорость башни, and dwell time affect tablet weight, толщина, разрушающая сила, и рыхлость. These relationships are interconnected and formulation-dependent, so manufacturers should evaluate the four attributes together rather than optimize them independently.
Understanding tablet CQAs means controlling the Critical Process Parameters (CPP) on the tablet press. Key CPPs include fill depth (die fill volume), main compression force, скорость башни (press output rate), and dwell/pre-compression settings. Table below (from JinLu’s reference guide) summarizes how each parameter influences tablet quality:
| Параметр | Technical Meaning | Влияние на качество планшета | Поиск неисправностей |
| Fill Depth (Объем) | Depth of powder in the die before compression | Sets tablet weight (доза) и толщина; key source of weight variation | Incorrect feeder cam or poor powder flow causes weight shifts. Adjust cam profile or improve flow. |
| Основная сила сжатия | Punch pressure (кН) exerted on tablet | Directly increases hardness and density; higher force generally lowers рыхлость. Too much force can cause capping or lamination. | Если таблетки слишком мягкие, raise force; if capping occurs, reduce force or add pre-compression. |
| Время пребывания (Compression Duration) | Time powder is under pressure (related to press speed) | Longer dwell (slower speed or twin-stage press) improves interparticle bonding and hardness. Very short dwell at high speed risks poor compaction (укупорка). | Slow down press or use two-stage (pre-comp) if tablets split or are weak. |
| Скорость башни (об/мин) | Rotation speed of the turret | Increases output but can degrade quality if too fast. High speed reduces fill time and can worsen weight uniformity and hardness consistency. | Balance speed with powder flow. Slow down if weight/hardness fluctuate. |
| Предварительная сжатие | Initial low-force compression before main press | Helps remove air and make a more uniform tablet core. It generally увеличивается final hardness and reduces capping/friability. | Add or adjust pre-compression if capping or lamination occurs (allows trapped air to escape). |
These relationships mean, например, что увеличение силы сжатия will raise hardness and lower friability (good up to a point). Однако, pushing force too far risks tablet failure modes (ламинирование, tool wear). Наоборот, changing the fill depth (to control weight) will shift thickness and may alter hardness indirectly. Как показывает таблица, setting each parameter requires balancing trade-offs, and troubleshooting often involves small tweaks (например. “try 1–2 kN more force” or “add a second compression stage” until tablets meet spec).
На практике, you usually optimize one attribute at a time, while monitoring the others. Here’s a practical sequence to balance the four key CQAs:
Throughout this optimization, good communication with formulation жизненно важно. Например, if you find you need excessive force to hit hardness, you might ask R&D to boost binder or granule density. If weight variation persists, consider re-granulating the blend for better flow. By following this sequence – fix weight, set hardness, validate friability, tweak thickness – you ensure the core quality needs are met first, then polish the tablet robustness.
Even with careful planning, дефекты планшета happen. Here are common issues and quick fixes, organized like a decision tree:
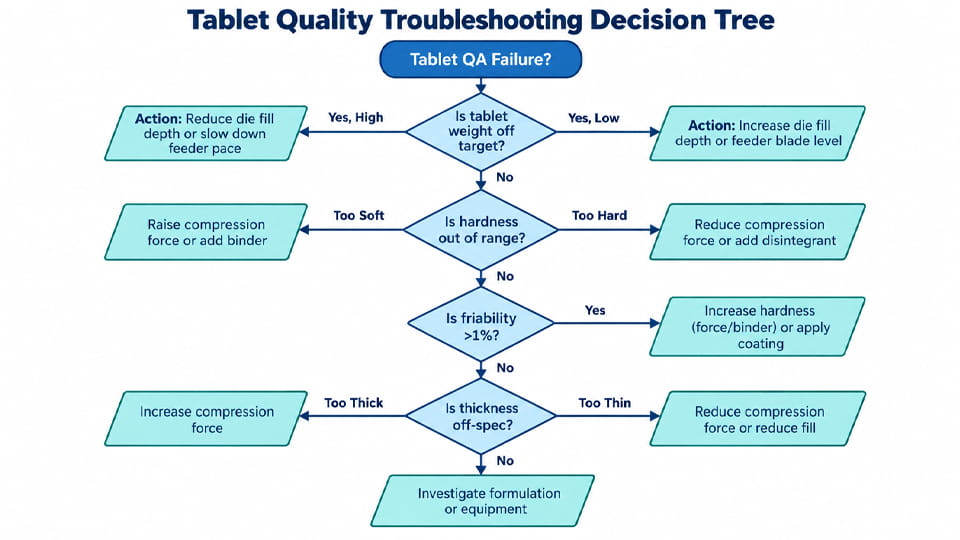
Interpretation: First check weight and thickness. High weight usually means overfill – reduce fill depth. Low weight means underfill – raise it. If weight is good, look at hardness. Мягкий (низкая твердость) tablets need higher force or formulation tweaks (больше связующего). Very hard tablets can cause downstream issues (like slow dissolution), so you might back off force or tweak disintegrant. If hardness is okay, test friability. Рыхлость >1% typically means surface bonding is weak, so increasing hardness (сила) or applying a thin coating can help. Окончательно, check thickness: overly thick tablets often mean under-compression, so increase force; too thin suggests over-compression or excessive fill. Each step should be followed by a small batch check to confirm the fix.
Кроме того, be alert for mechanical defects common on a press:
Remember that hardness and friability are critical ниже по течению QC checks, not just in-compression values. Жесткий, durable tablets are easier to coat and package without breaking. Например, high friability means tablets will shed dust and chips in a coating pan or on packaging lines, causing visual defects and yield loss. Наоборот, a tablet with the right hardness but uneven thickness could lead to over- or under-application of coating solution or inconsistent Блистерная стакана сжатие.
На практике, ensuring tablets have acceptable weight and strength beforehand streamlines coating. Tablets that meet hardness and friability specs typically survive the rigors of coating (spray and tumbling) and automated packaging. Наоборот, if tablets are too soft (низкая твердость), you will see breakage and dust in the coating pan; too hard (Высокое сжатие) might mean incomplete film formation (coatings may crack). В идеале, tablet thickness should also be uniform so that coating weight is even. The Jinlu case study notes that “hardness (разрушающая сила) checks internal strength, while friability checks surface durability… Both properties affect downstream processing – from how tablets are compressed to how they are coated and finally packed.”. Другими словами, always consider these attributes in the context of the whole line: a tablet that fails packing (broken pieces) or has streaked coating is often a symptom of poor compaction quality upstream.
Modern rotary tablet presses are built with features that make balancing these CQAs easier:
By leveraging these machine features — automatic weight adjustment, предварительное сжатие, forced feeders, and servo feedback — a production line can maintain consistent tablet CQAs even under stress (высокоскоростной) or raw material variability. The net effect is fewer out-of-spec tablets and smoother coating/packing later on.

Balancing tablet weight, твердость, thickness and friability is a classic Quality-by-Design challenge. By understanding how raw materials and compression settings drive each quality attribute, you can set up a robust control strategy. Use in-process checks on weight, твердость, and thickness to detect drift early, and perform the official friability test on finished batches to verify mechanical durability. Современный Роторные таблетки прессы (like the JinLu ZP-series) offer features — servo-driven cam control, weight-feedback, two-stage compression, forced feeders — that make this balancing act much easier.
Ready to streamline your tablet production? Связаться с ДжинЛу Упаковка to explore our high-performance ротационные таблеточные прессы, equipped with automatic weight control and compression monitoring. We can arrange sample testing on your formulation to optimize your tablet quality attributes.
Фармакопеи (like USP) require each tablet be close to the average weight. A common spec is that no more than 2 из 20 tablets can deviate outside ±5% of the average (для планшетов >80мг). For very small tablets (<80мг), the limit is ±10%. Однако, your own specification may be tighter depending on the API dose and potency. Always refer to USP or for your dosage form.
Твердость таблетки (разрушающая сила) is measured by a hardness tester (manual or electronic). The tester compresses a single tablet until it cracks, reporting the peak force (in kg or Newtons). Modern digital testers often record diameter and thickness at the same time. According to USP , you take an average of multiple tablets and set a min/max range. В производстве, hardness is usually monitored continuously and adjusted via the press settings as needed.
Первый, reduce the compression force in small steps. Also check if you can decrease binder (or increase disintegrant). Very high hardness can slow dissolution or make tablets hard to swallow. After adjusting, always re-test friability and disintegration.
High friability usually means tablets are under-compressed or poorly bonded. Increase tablet hardness by raising compression force or improving formulation (больше связующего, грануляция). Adding a thin film coating often solves minor friability, but the root is densification. Also ensure you have adequate dwell/pre-compression time to fully consolidate the tablet.
Да. Different shapes (round vs oblong, single vs double convex) distribute compression force differently. Например, very thick or tall tablets tend to be harder, whereas thin tablets may need less force. If you change tooling or die dimensions, you should re-qualify the fill and force settings. Always measure thickness for new tablet shapes, and watch how that impacts hardness and friability in trials.
It depends on regulatory guidance and risk. Обычно, Вес таблицы (or content) is sampled at least every hour (or more frequently) during a run. Hardness and thickness can be spot-checked similarly (например. 3–5 tablets per shift) or even continuously on-line if you have automatic testers. Friability is usually checked on a full batch at release. Good practice is to set in-process controls for weight and hardness with acceptance criteria, and only do friability at the end (since it’s destructive).
Ensure the blend has good flow (consider slugging or granulation if not). Adjust the feed frame height and paddle, or use a forced feeder. Check the punch and die alignment. If variation persists, a servo press can actively control weight via a feedback loop. В итоге: improve flow + fine-tune feeder cam.
The USP chapters are (Weight Variation/Content Uniformity), (Tablet Breaking Force, то есть. Твердость), и (Таблетка хрупкость). These give standard methods (like number of tablets, rotation count for friability, и т. д.). We follow those protocols in our QC lab. Например, USP friability test is described in JinLu’s resource.
Ссылки:
1.я Q8 (Р2) Pharmaceutical development —— Европейское агентство лекарственных средств
2.Управление рисками качества —— я Q9(Р1)
3.Pharmaceutical Quality System —— ICH Q10
4.Tablet Compression Force as a Process Analytical Technology (ПАТ): 100% Inspection and Control of Tablet Weight Uniformity —— ПабМед
5.Tablet disintegration performance: Effect of compression pressure and storage conditions on surface liquid absorption and swelling kinetics ——ПабМед
6.Единообразие дозировок —— USP <905>