
で 医薬品ブリスター包装, the thickness of the formed cavity wall is an important quality parameter. Although the incoming PVC, PVC/PVDC, or other thermoformable film may meet its original thickness specification, the material becomes thinner when heated and stretched into blister cavities. 結果として, different areas of the same cavity can have significantly different wall thicknesses.
Blister thickness measurement after forming helps manufacturers identify local thin spots, evaluate thickness uniformity, and determine whether the formed packaging can meet its mechanical and protective requirements. Simply checking the nominal thickness of the incoming film is not enough to confirm the quality of the finished blister.
The key is to measure the right locations, use an appropriate testing method, and establish acceptance criteria based on 材料特性, キャビティの形状, そして 包装性能. This guide explains where blister walls tend to become thinner, how to measure formed blister thickness, how to design a practical sampling plan, and how to improve thickness consistency during production.
Thermoforming stretches the plastic film into cavities, unavoidably thinning it. Imagine heating a flat PVC sheet (say 250 μm thick) and pulling it into a deep pocket: the film must cover more surface area than it started with, so it gets thinner. 実際には, the average final wall thickness equals the original thickness divided by the areal draw ratio (final area ÷ original area). 例えば, if the drawn blister has twice the surface area, the average thickness is roughly half the starting gauge.
Film thinning is an “inescapable physical reality” in thermoforming. This thinning effect is influenced by the draw ratio (深さ対. オープニング), part geometry, 加熱, and forming method. For shallow draws (small depth), thickness might only drop 10–20%. But deep-draw blisters (depth roughly equal to width) can see wall thickness reductions of 50% 以上.
Practical reasons to gauge forming thickness include:
Standard thickness specs like ISO 4593 or ASTM D6988 exist for flat films, but note: those apply to unformed specimens, not embossed or formed parts. 例えば, ISO 4593 explicitly states the mechanical scanning method “is not suitable for use with embossed film or sheeting”. 言い換えると, there is no ISO rulebook for “blister cavity thickness of the month.” We must measure formed walls ourselves and set limits from first principles (material specs, draw ratio calculations, product tests, 等). 持ち帰り: don’t assume the sheet thickness spec covers the formed wall – measure it.
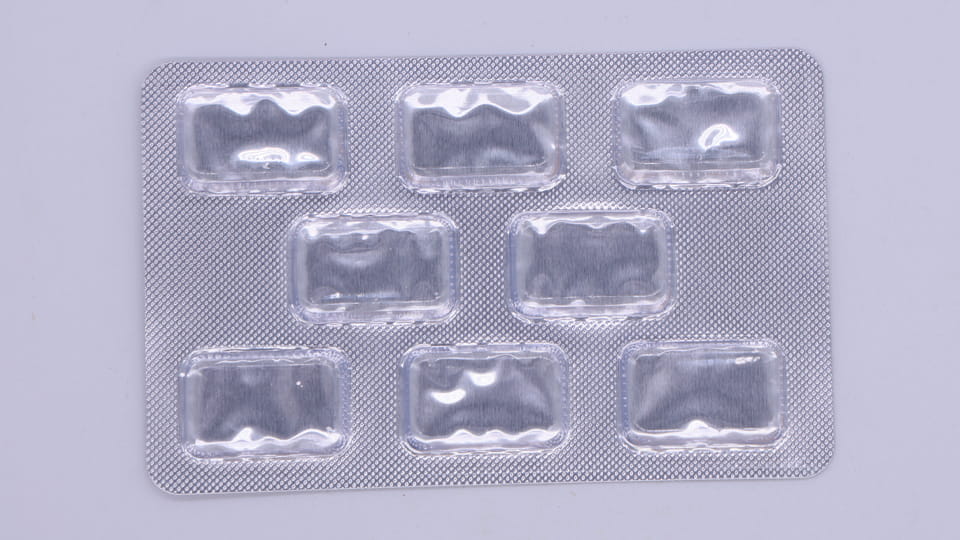
Certain areas in a thermoformed blister tend to thin more than others. 一般的に, の deepest stretching zones end up thinnest, while un-stretched or lightly-stretched zones stay near the original gauge. Industry sources note a predictable pattern:
Keep in mind these are typical trends, not absolutes. The exact “weak points” depend on the specific キャビティの形状, 延伸倍率, そして forming conditions. 例えば, a square cavity might have very sharp corner thinning, while a round cavity spreads the stretch more evenly. One blister design guide emphasizes that cavity dimensions and corner radii directly affect thin spot formation. 実際に, you often find the thinnest film at the hardest-to-form spot – usually sharp internal corners or the deepest draw.
Measuring the formed wall thickness requires precision tools and careful sample prep. There are a few common approaches:
In everyday QC, ある digital thickness gauge or micrometer is most common. 例えば, a 0–12.7 mm digital gauge with 0.01 mm resolution can measure plastic films accurately. You simply lower the probe onto the cross-section. 鍵となるのは、 make flat, perpendicular cuts through the blister (using a scalpel or circular saw) so the gauge touches the true wall surface without bending it.
When taking measurements, ensure the tool is zeroed, the film is clean, and cut edges are perpendicular and undistorted. If a blister film is multilayer (のように PVC/PVDC), remember you measure total thickness. You might average multiple readings at one point (gently lift and remeasure) to ensure consistency. Always note the measurement locations and conditions.
実際に, no single standard covers “finished blister thickness measurement for QC.” For instance, ASTM D6988 – a guide for film specimen thickness – explicitly says it しません cover sampling or QC methods for finished products. So your methods and criteria are typically defined in-house or by material specs. What’s important is accuracy and consistency in your measurement method.
A critical part of thickness control is sampling at the right spots. Blister cards are large sheets that span the film width and run through the machine, so variation can occur in two directions: across the sheet (cross-web) and along the machine direction (infeed to discharge). A risk-based sampling plan should cover both dimensions and multiple cavities.
Consider sampling in these ways:
例えば, a QA team might measure thickness at left/middle/right on the first, middle and last card of a run, and within each of those cards measure 4 corners, 4 sidewalls, and the bottom. The exact sample count isn’t fixed by regulation; it’s typically based on an AQL or process capability decision. 鍵となるのは、 span the whole sheet and process so you spot any pattern (例えば. one side consistently thinner, or end of run drift).
Think of the sampling layout like a grid:
重要なこと, treat your sampling plan as risk-based: focus on high-shear or deep-draw features. If a certain cavity or track is known to be marginal, include it every run. If new tooling or material is introduced, be more aggressive in sampling (例えば. measure more points or cards). There is no one-size-fits-all minimum; whatever you do should be documented and consistently followed.
There is no single universal “cookbook” for acceptable wall thickness in blister packs. Each product and material can be different. しかし, here are guiding principles for setting criteria:
Be careful not to just copy flat-film tolerances. A blister cavity is like a different product than the flat sheet it started from. 例えば, ISO 4593 and ASTM D6988 specify film measurement methods but explicitly do ない define pass/fail criteria for formed products. There is no ISO or ASTM standard that says “blister corner wall must be at least X μm.” Instead, use those as reference for gauge accuracy, and establish your own spec.
One practical rule: if the 平均 wall thickness (across all measured points) stays near the expected value (例えば. within 5–10%), そして 最小 thickness at the most-stretched point meets your design requirement, you’re likely in good shape. 例えば, some quality groups accept blisters if all measured walls are within ±10–15% of the average thickness, and no corner is below a set fraction of nominal.
ついに, document whatever criteria you choose in a QC procedure. Make it clear which points are critical, what statistical bounds apply, and what to do if a batch fails. 例えば, you might say: “Accept batch if ≥95% of measured points are ≥80% of nominal film thickness, and corners ≥75 μm” – based on your validation data. Always support criteria with a risk assessment or test evidence.
(注記: An illustrative acceptance table might list “Nominal = X μm, Tolerance ±Y μm, Minimum corner = Z μm, 履歴書 < 15%”, 等, but values depend on your product.)
Knowing what makes walls uneven helps you avoid thin spots in the first place. Common causes of thickness variation include:
要約すれば, any feature or setting that forces the film to “pull farther or faster” will create thin spots. Manufacturers often emphasize that excessive draw ratio is the root cause: if your design requires an extreme stretch, even thick film will thin out (and may tear).
Environmental factors like ambient humidity have little effect on film thickness (though moisture can affect strength or lamination). Tension control on the web can matter: too high tension can over-stretch the film into the pocket; too low can cause wrinkles and local thick spots. But tooling and heat are usually bigger drivers of uniformity.
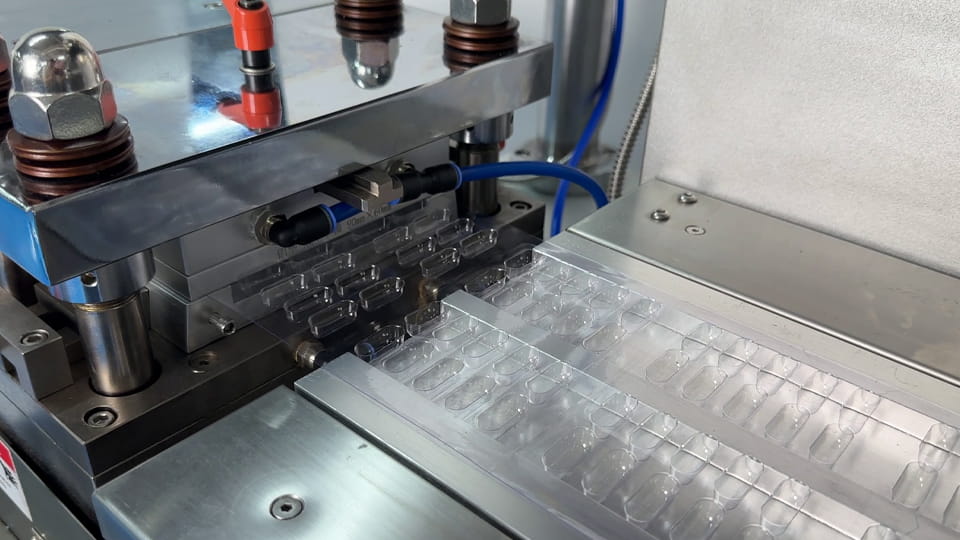
If measurements show problematic thin zones, there are several levers to pull:
Whenever you make a change, re-qualify. 例えば, if you add plug-assist, re-measure the formed thickness to ensure corners improved. 原則として, “try the design/process fix, then re-form and measure before approving”.
To keep measurements reliable, follow a consistent procedure. Here is a sample checklist for each thickness check session:
By following a disciplined QA routine, you ensure measurements are consistent day-to-day. Any trends (例えば. gradual thinning of all cavities over time) become visible in the records, prompting preventive action.
Measuring blister wall thickness after forming is essential for ensuring blister pack quality and patient safety. The formed walls can be much thinner than the raw film (sometimes only a quarter of the original at sharp corners), so targeted thickness checks catch potential weak spots. Key takeaways: use proper gauges or microscopy to measure cut samples (recognizing that ISO standards cover only flat film), sample strategically across the card, and define acceptance based on design needs rather than guesswork. Focus on the minimum local thickness at critical points and maintain a realistic tolerance (often ±10–15% around nominal average). Remember that no single standard governs blister thickness – you must tailor your criteria to the specific materials and product.
If you encounter persistent thin spots or variability, look upstream: review your blister cavity design, 延伸倍率, heating uniformity, and consider process aids like plug-assist. Improving uniformity often comes down to better mold design and process control, not just more expensive film.
For pharmaceutical manufacturers evaluating ブリスター包装装置, the forming station, heating system, mold design, and material-handling configuration all deserve attention. Jinlu Packing provides pharmaceutical blister packaging machinery solutions designed to support efficient and consistent packaging production. 私たちのチームに連絡してください to discuss your blister packaging requirements and equipment options.
Formed blister thickness can be measured using a suitable digital thickness gauge or micrometer on accessible areas. Cross-sectional microscopy is useful for detailed measurement of curved cavity walls, corners, and other critical locations. The method should be validated for the material and sample geometry.
Thermoforming heats and stretches plastic film into a cavity. As the material covers a larger surface area, its thickness decreases in stretched regions. The degree of thinning depends on cavity geometry, 延伸倍率, 材料特性, heating conditions, and forming method.
The thinnest point depends on the cavity design and forming conditions. Deep corners, sidewalls, and bottom transitions are common areas requiring attention. Manufacturers should perform thickness mapping to identify the actual minimum-thickness location rather than assume one fixed location is always thinnest.
Common causes include excessive cavity depth, 鋭い角, uneven heating, improper vacuum distribution, and inadequate plug-assisted forming. Material properties and web alignment can also influence thickness distribution.
There is no universal minimum wall thickness for all pharmaceutical blister materials and cavity designs. Manufacturers should establish minimum local thickness requirements using material specifications, キャビティの形状, mechanical performance, and appropriate packaging validation data.
The number of measurement points depends on cavity geometry, プロセスリスク, and validation results. A thickness-mapping study should initially cover critical areas such as corners, sidewalls, and the cavity bottom. Routine inspection can then focus on the locations identified as most critical.
はい, provided the measuring instrument can properly contact the intended surface without compressing or deforming the sample. Conventional micrometers may not be suitable for small or sharply curved cavity locations. Cross-sectional microscopy can be used when more detailed measurements are required.
Incoming film thickness refers to the thickness of the original flat material before forming. Formed blister thickness refers to the local wall thickness after the material has been heated and stretched into the cavity. The two values can differ considerably because of material redistribution during thermoforming.
Greater cavity depth generally increases the amount of material deformation required during forming. Depending on cavity geometry and forming conditions, this can increase local thinning in the sidewalls, corners, or bottom regions.
Manufacturers can improve thickness consistency by optimizing heating conditions, reviewing cavity geometry, adjusting plug-assisted forming where applicable, maintaining vacuum and pressure systems, and controlling web tension and alignment. Thickness should be remeasured after process changes to verify the results.
参考文献:
1.Plastics — Film and sheeting — Determination of thickness by mechanical scanning —— ISO 4593:1993
2.Standard Test Method for Determining Plastic Film Thickness and Thickness Variability Using a Non-Contact Capacitance Thickness Gauge —— ASTM D8136-24
3.Evaluation of the Thickness and Oxygen Transmission Rate before and after Thermoforming Mono- and Multi-layer Sheets into Trays with Variable Depth —— MDPI Polymers
4.熱成形における肉厚分布の決定におけるプラグ設計の役割 —— ワイリーオンラインライブラリ
5.Oxygen barrier properties of Thermoformed trays manufactured with Different Drawing methods and Drawing Depths —— ワイリーオンラインライブラリ
6.Determination of the thickness of plastic sheets used in blister packaging by near infrared spectroscopy: development and validation of the method —— サイエンスダイレクト