Your máquina de contagem de gomas ran well on the last order. Then a new bottle or gummy arrived, and operators started clearing the funnel.
For supplement contract manufacturers, this problem reaches beyond the filling station. Production managers lose scheduled output. Operators spend time clearing blockages. Downstream cappers and labelers wait for bottles.
A gummy counter must do more than register pieces. The product must also pass through the discharge path and enter the bottle.
Before you replace a funnel or reduce speed, check where the flow changes. The blockage may start before the bottle neck.
Fabricantes contratados rarely control every detail of a customer’s specification. A new order can change several filling conditions at once.
Custom gummies can vary in thickness, forma, firmness, and surface condition. A setting that works for small pieces may struggle with larger products.
Custom gummy bears also need checks for their widest dimensions and orientation. Bear shapes cannot be assessed by length alone.
Compare actual production samples, not just drawings. Check whether pieces remain separate after storage and handling. Note any coating residue.
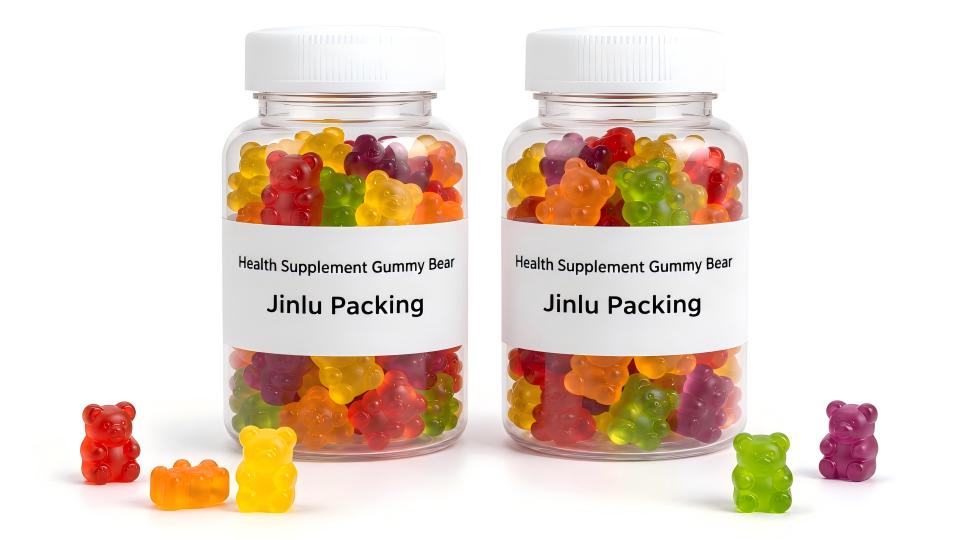
Brand specifications for custom gummy packaging may include a large bottle with a narrow opening. Internal volume does not establish filling clearance.
For a gummy bear package, check the neck’s internal diameter and the shoulder profile. Bottle body diameter provides insufficient information.
Your gummy packaging assessment should link the container to the actual product. Neither can be approved in isolation.
A higher count per bottle means more pieces must pass through the same opening during each filling cycle.
The gummy counting machine may need different settings or discharge components. Verify the new combination before scheduling its production rate.
A gummy bottle neck blockage is visible at the outlet. Its cause may include uneven feeding farther upstream.
Watch the product before it reaches the counting area. Does it move as separated pieces, overlapping layers, or sticky clusters?
A sudden surge increases demand on the discharge path. Pieces can also gather again after counting, even after passing sensors separately.
Film the full route through your gummy counting machine. A close-up of the bottle alone can miss the first buildup.
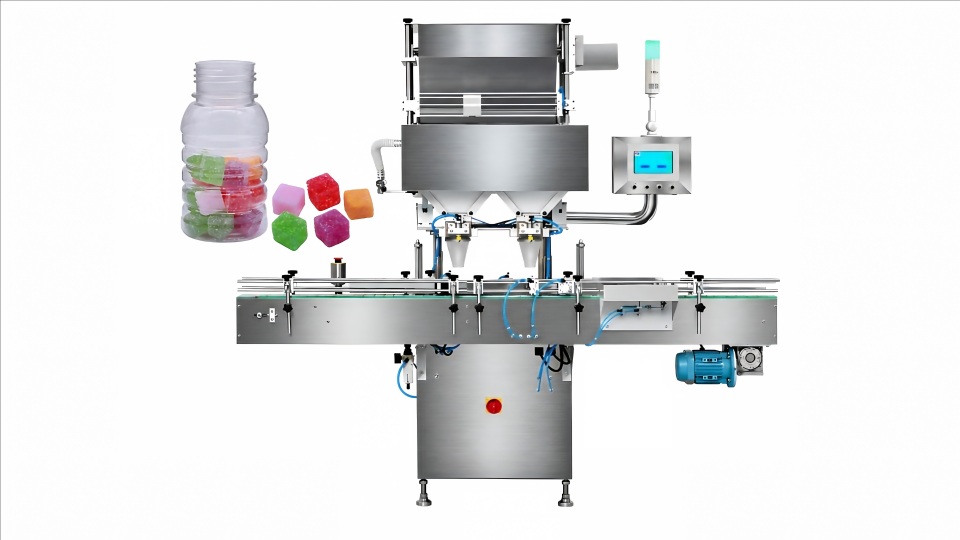
Our JL-DSL-16R uses hopper agitation, rolos de separação, and feeding mechanisms to help distribute gummies before counting.
These features matter when incoming products tend to gather in groups. They address product presentation before the funnel receives the material.
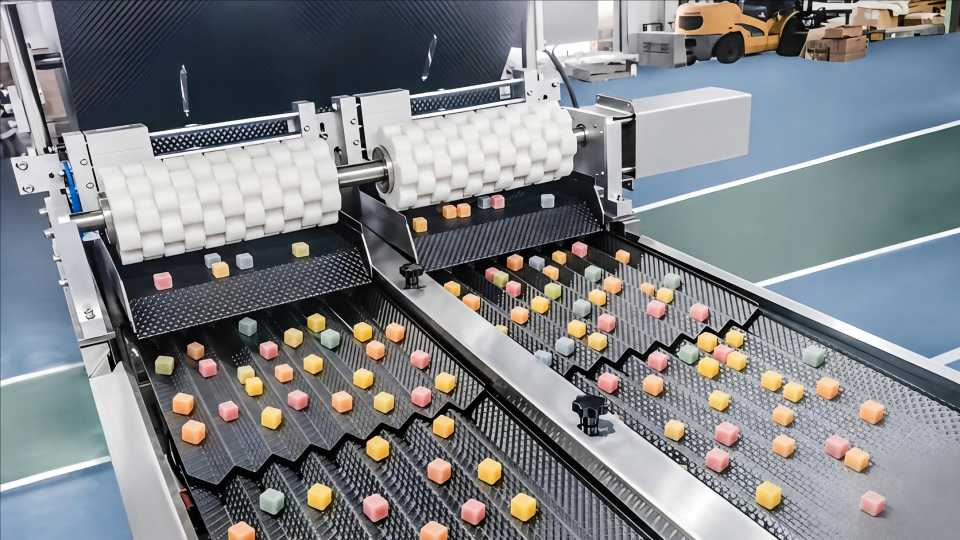
The JL-DSL-16R has textured, PTFE-coated vibratory channels and a stepped track arrangement. Vibration adjustment helps match feeding to product behavior.
These features aim to reduce surface adhesion and improve distribution. Actual results depend on the gummy and its operating conditions.
This is why a gummy packaging machine needs assessment beyond its lane count. Product handling affects what reaches those lanes.
A tablet counting machine or capsule counting machine may handle some free-flowing gummies. Confirm separation and discharge performance before choosing one.
No gummy counting machine can compensate for every incoming product condition. Severely bonded clusters require a review of product preparation and storage.
If separated gummies still stop near the outlet, examine the funnel, the neck opening, and the timing of product release.
You may see gummies bridging in the filling funnel. Several pieces support one another across a narrow passage.
More product then collects above them. Surface tack can make that obstruction harder to clear.
This explains why faster counting does not always produce faster bottling. The next stage must accept the product at that rate.
Our JL-DSL-16R uses an enlarged PTFE vibratory discharge structure. PTFE helps reduce adhesion at the contact surface.
The discharge geometry provides space for product movement. Vibration helps material travel through the discharge area.
When comparing a gummy candy packaging machine, inspect this section under continuous operation. Look for growing residue, repeated hesitation, and manual intervention.
These observations provide stronger evidence than an unsupported promise of jam-free operation. Test your material under the agreed production conditions.
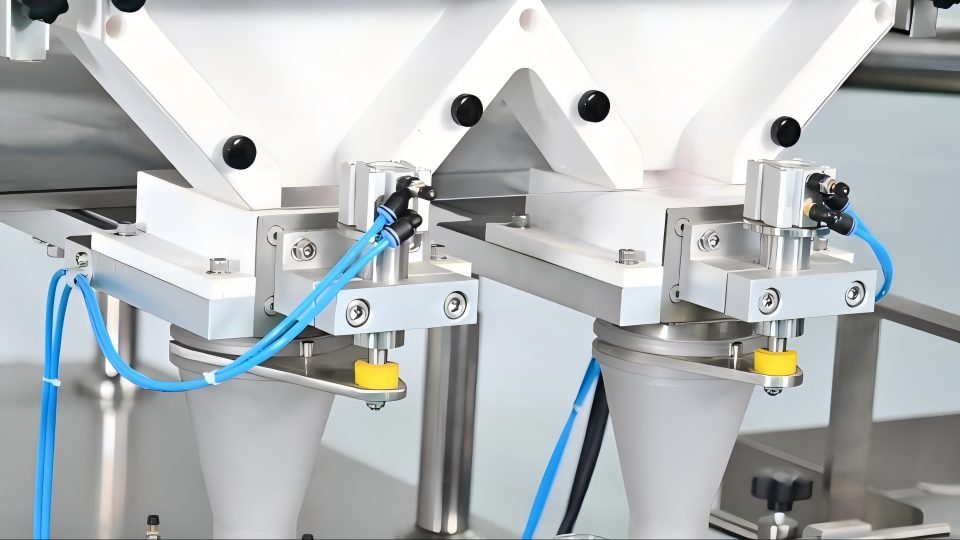
A gummy filling funnel must suit both the product and the bottle. Its inlet, transition, and outlet all affect passage.
Our funnel sizing follows the bottle opening, with product suitability checked during trials. A larger funnel alone does not resolve every restriction.
If you compare a gummy bear packaging machine, test the actual bear shape through the proposed outlet. Do not approve fit from bottle capacity.
For gummy candy packaging, photograph the bottle neck and provide internal dimensions. Include the product’s length, largura, e espessura.
An appropriate opening still needs correct positioning. Check alignment if pieces strike the rim or fall outside the container.
Watch whether the bottle settles under the funnel before discharge. Check for movement during filling and premature release afterward.
Our JL-DSL-16R uses dual positioning cylinders to help locate bottles at the filling station. Settings still need confirmation after bottle changes.
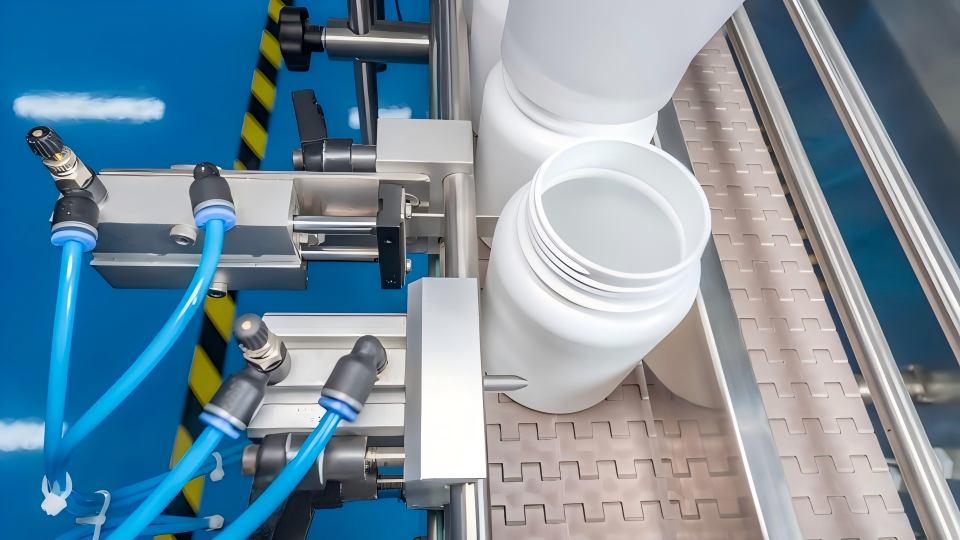
Positioning addresses the relationship between the bottle and outlet. It does not remove gummy tack or replace suitable funnel geometry.
Da mesma maneira, an independent photoelectric module cannot correct a displaced bottle. Diagnose each part of the gummy counter according to its function.
This distinction helps maintenance teams choose relevant adjustments. It also prevents repeated sensor changes when the fault occurs farther downstream.
For multi-SKU factories, gummy packaging performance also depends on changeovers. Residue and reassembly deserve checks before the next batch starts.
The JL-DSL-16R has modular components and a channel locking arrangement for disassembly. Inspect access around channels, funis, and gates.
The supplied specification lists 316L stainless steel and suitable engineering plastics for product-contact parts. Confirm materials in the agreed configuration.
Assess hygienic design through practical inspection. Can operators reach residue locations? Can they remove components and reinstall them correctly?
Review easy disassembly and easy cleaning against the actual cleaning procedure. Do not assume removable parts permit every washing method.
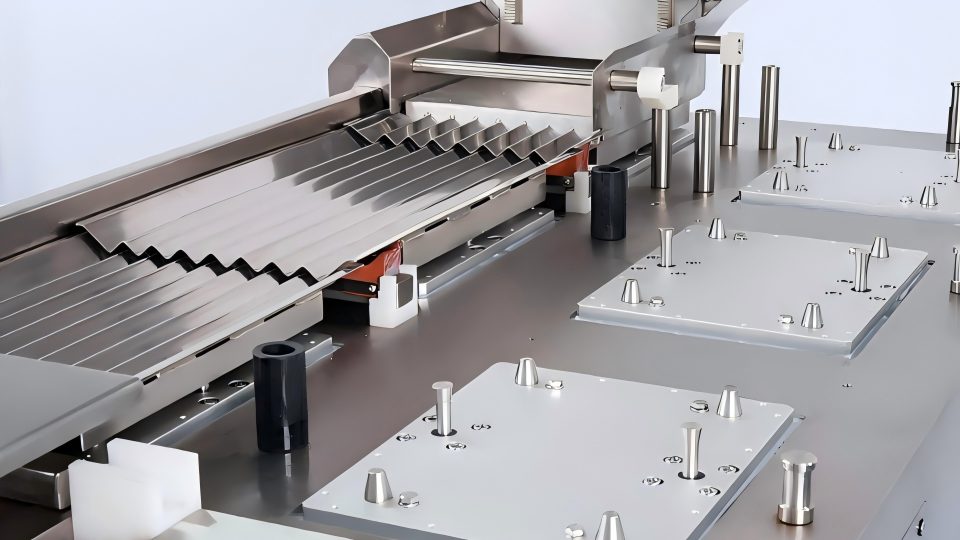
For GMP-oriented design, discuss cleaning access, material identification, and cross-contamination control. Equipment features must fit your site’s procedures.
Ask about the product-contact parts list, cleaning procedure, and maintenance procedure. Confirm which documents the supplier can provide.
A vitamin gummy packaging machine needs evaluation against the customer’s product and quality requirements. A broad certification phrase cannot replace that review.
The useful comparison is sustained output from your gummy counting machine, including interruptions. A short display of peak speed tells only part of the story.
Include a routine product and the most difficult SKU you expect to run. Use actual bottles, conta, and target speeds.
For a gummy vitamin packaging machine, include the bottle specified by the brand. A convenient demonstration bottle may conceal a fit problem.
Agree on a trial duration that can reveal residue buildup and repeated interventions. Record adjustments and any required component changes.
Use the following table during acceptance testing. Check physical filling behavior and bottle quantities separately.
| Test area | What to record |
| Gummies and bottles | Gummy dimensions, surface condition, internal neck diameter, and count per bottle |
| Operating conditions | Target speed, actual speed, and trial duration |
| Bottle entry | Blockages, retained pieces, derramamentos, and their locations |
| Operator intervention | Number and duration of clearing, limpeza, and adjustment actions |
| Filling results | Bottle count checks, acceptable bottles, and nonconforming bottles |
Calculate accepted bottles over the full trial period. Include stops in that period, and record how many bottles received quantity checks.
Define a Factory Acceptance Test (GORDO) around the agreed product and bottle combinations. Set measurable criteria before the test begins.
Após a instalação, plan a Site Acceptance Test (SENTADO) for local conditions and line connections. Confirm both test scopes with the supplier.
Our gummy counting machine can connect with bottle unscrambling, inserção dessecante, limite, vedação por indução, e equipamento de etiquetagem.
Confirm the ordered modules, interfaces, and sustained line rate. Individual station ratings do not establish the output of the assembled line.
Broader searches for packaging for gummies cover bottles, bolsas, Materiais, e máquinas. Narrow the requirement before comparing equipment.
If you ask how to package gummy bears, start with the sales specification. Confirm piece count, bottle choice, encerramento, and product condition.
Then test separation, contando, bottle entry, and downstream handling. This article addresses that bottle-filling route, rather than pouch sealing.
How are gummy bears packaged? The answer depends on the chosen format. For counted bottles, product preparation comes before counting and filling.
Closure, vedação, and labeling follow as specified. Gummy bear packaging equipment must match that route and the required checks.
Which gummy counting machine for sticky gummies should you shortlist? Examine separation, superfícies de contato, discharge geometry, positioning, and cleaning access.
For projects described as edible gummy packaging, first define the product and container. That phrase alone does not establish machine suitability.
The JL-DSL-16R offers structures worth testing against those needs. Sample results should decide whether it fits your production requirements.
Send us your gummy dimensions, surface condition, bottle neck measurements, and shoulder photographs. Include count per bottle and target bottle speed.
If your current gummy packaging line jams, share a video from feeding through bottle entry. Identify the hardest product in your order mix.
We can assess the JL-DSL-16R configuration and funnel fit with you. Test your samples before selecting a gummy counting machine for the next order.
A gummy counting machine may handle several products, but each combination needs testing. Custom gummies can differ in size, forma, firmness, e revestimento.
Our JL-DSL-16R combines separation rollers, coated vibratory channels, and a PTFE discharge structure. These features help manage product flow. Trials should confirm the settings, funnel requirements, and achievable bottle speed for each representative SKU.
A narrow opening can restrict product flow, even when the bottle has enough internal capacity. Several pieces may gather across the opening and cause a gummy bottle neck blockage.
The gummy filling funnel should match both the gummy dimensions and the bottle neck. For the JL-DSL-16R, we assess funnel fit using bottle specifications and actual product samples. Bottle positioning also needs verification.
Actual output depends on product separation, discharge behavior, bottle positioning, e equipamentos a jusante. The counting rate alone does not establish the finished bottle rate.
Test your gummy counter at the required count per bottle. Record acceptable bottles, para, derramamentos, and operator interventions over the agreed trial period. This provides a practical basis for production planning.
Before a new gummy packaging run, check channels, gates, and funnels for residue. Confirm that cleaned components are dry and correctly installed.
The JL-DSL-16R has modular components that support disassembly and cleaning access. Follow the agreed cleaning procedure and confirm material compatibility. After reassembly, check alignment and verify bottle quantities before releasing production.
Send a routine product and the most difficult SKU planned for your gummy packaging machine. Include actual bottles and closures, plus product dimensions, surface condition, velocidade alvo, and count per bottle.
For custom gummy bears, include samples that represent normal production variation. If your current line jams, send a video from feeding through bottle entry. These details help us assess the JL-DSL-16R configuration and trial requirements.
Referências:
1.21 C.F.R. § 111.27—What requirements apply to the equipment and utensils that you use? (n.d.). Código Eletrônico de Regulamentações Federais. Retrieved November 16, 2026
2.21 C.F.R. § 111.30—What requirements apply to automated, mecânico, or electronic equipment? (n.d.). Código Eletrônico de Regulamentações Federais. Retrieved November 16, 2026
3.Comissão Europeia. (2015, Marchar 30). EudraLex, Volume 4: EU guidelines for good manufacturing practice —Annex 15: Qualification and validation.
4.NÓS. Food and Drug Administration. (2010, dezembro). Small entity compliance guide: Current good manufacturing practice in manufacturing, embalagem, rotulagem, or holding operations for dietary supplements.